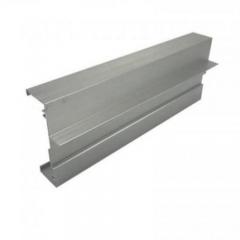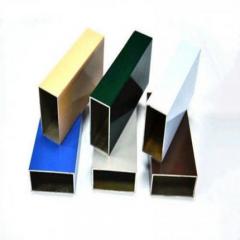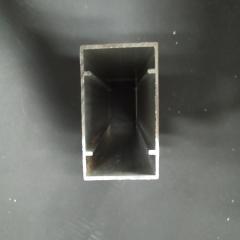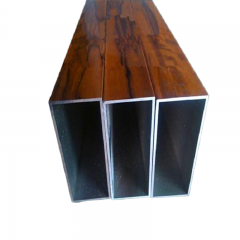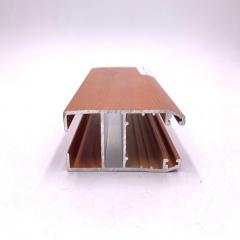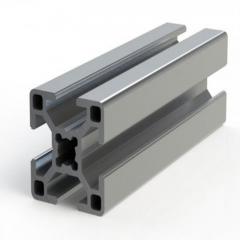
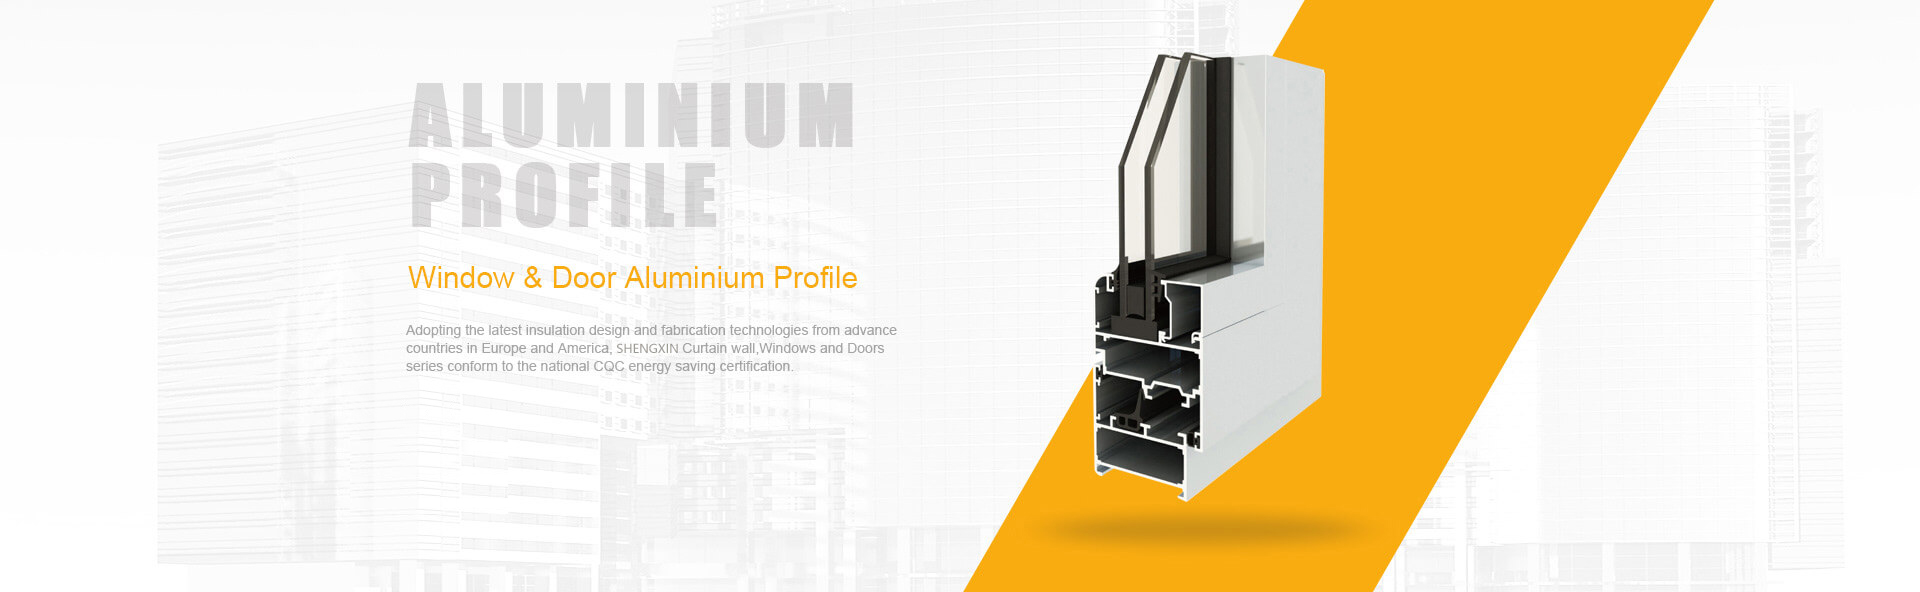
Ever wondered how manufacturers create those intricate aluminum shapes you see in everything from window frames to industrial machinery? The answer lies in a fascinating process called aluminum extrusion. Custom aluminum extrusion profiles are specially designed cross-sectional shapes created by forcing heated aluminum alloy through a steel die—much like squeezing toothpaste through a tube, but with far more precision and engineering behind it.
Aluminum extrusion is a manufacturing process where aluminum alloy is heated and forced through a shaped die opening to create continuous profiles with consistent cross-sections, enabling the production of complex geometric shapes impossible to achieve through other metalworking methods.
So what is extrusion aluminum exactly? It refers to any aluminum product created through this die-forming process, resulting in profiles that maintain their cross-sectional shape along their entire length. The beauty of this method lies in its ability to produce remarkably complex geometries in a single, efficient operation.
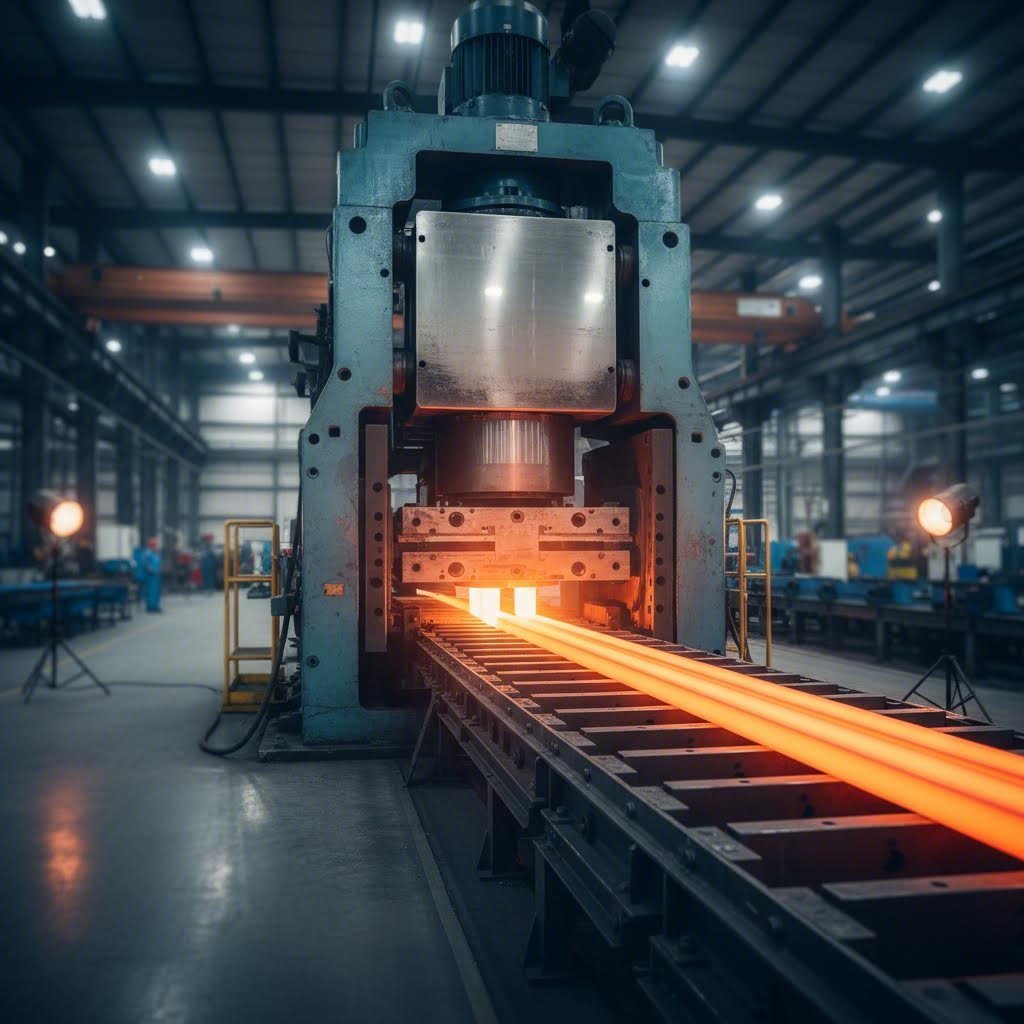
The journey from raw aluminum to finished aluminum profile begins with a cylindrical billet—a solid log of aluminum alloy. This billet is heated to approximately 800-925°F, making it malleable enough to flow through the die opening. A powerful hydraulic ram then pushes the softened metal through the precision-cut die at controlled speeds.
As the aluminum emerges from the die, it takes on the exact shape of the opening—whether that's a simple rectangular tube or an intricate multi-chambered design with internal walls, channels, and mounting features. The extruded aluminum then moves along a runout table where it cools, gets stretched for straightness, and is cut to specified lengths. This aluminium extrusion process can create profiles ranging from tiny heat sink fins to massive structural components.
Standard stock aluminum extrusion profiles include common shapes like angles, channels, tubes, and T-slots that serve general-purpose applications. You'll find these extrusions readily available from distributors for quick-turnaround projects.
Custom-designed profiles, however, offer distinct advantages when your application demands specific performance characteristics:
Manufacturers choose custom aluminum extrusion profiles over off-the-shelf options when standard shapes simply cannot deliver the required performance, integration, or efficiency. Imagine designing an LED light fixture housing—a custom aluminum profile can incorporate the heat sink, mounting channels, lens retention features, and decorative trim all in one seamless piece. That's the power of application-specific extrusion design.
Choosing the right aluminum alloy for your custom extrusion project might seem straightforward—until you realize how dramatically material selection affects performance, finish quality, and manufacturing success. The 6000 series alloys dominate the extrusion industry for good reason: they combine excellent extrudability with the right balance of strength, corrosion resistance, and workability. But which specific alloy should you specify?
When evaluating aluminum profiles for custom applications, two alloys consistently rise to the top: 6063 and 6061. Both belong to the magnesium-silicon family, making them heat-treatable and well-suited for extrusion. However, their distinct compositions create meaningful differences in how they perform—and where they excel.
Think of 6063 as the "architect's alloy" and 6061 as the "engineer's alloy." This distinction captures their fundamental differences in a nutshell.
Aluminum 6063 contains approximately 98.9% aluminum with 0.7% magnesium and 0.4% silicon—a simpler, purer composition. This translates to superior surface finish capabilities, making it the go-to choice for anodized architectural applications. You'll often hear industry professionals call it "architectural aluminum" because extruded aluminum profiles in 6063 accept decorative finishes beautifully.
Aluminum 6061, by contrast, includes higher amounts of copper, silicon, chromium, and iron in its composition. According to Tri-State Aluminum's specifications, this more complex chemistry delivers excellent strength and machinability—but at the cost of finishing response. The Brinell hardness of 6061 reaches 95 compared to 6063's 73, indicating significantly greater structural capability.
Here's what these differences mean for your aluminium extruded profile decisions:
| Property | 6063 Aluminum | 6061 Aluminum |
|---|---|---|
| Tensile Strength (T6 temper) | ~30,000 psi | ~45,000 psi |
| Corrosion Resistance | Excellent | Good |
| Extrudability | Superior—handles intricate designs | Good—better for simpler shapes |
| Surface Finish Quality | Excellent—ideal for anodizing | Fair—poor finishing response |
| Machinability | Moderate | Good (50% rating) |
| Weldability | Excellent | Good with proper filler material |
| Typical Applications | Window frames, architectural trim, signage, furniture | Structural components, aerospace, machinery, heat sinks |
So how do you decide between these profile aluminum options? Start by asking three critical questions about your application:
What structural loads will the profile bear? If your aluminum extrusion profile must support significant weight or withstand high stress, 6061's superior tensile strength makes it the clear winner. Think structural framing, truck trailer components, or machinery enclosures. For decorative trim, cabinet components, or light-duty architectural elements, 6063 provides adequate strength with better finishing characteristics.
How important is surface appearance? Projects requiring high-quality anodized finishes, bright decorative surfaces, or consistent aesthetic appeal demand 6063. Its purer composition responds beautifully to anodizing, producing uniform, attractive results. If your extruded profiles will be hidden inside assemblies, painted with thick powder coatings, or used in purely functional applications, 6061's finishing limitations become irrelevant.
What environmental conditions will the profile face? Both alloys resist corrosion well, but 6063's lower copper content gives it an edge in harsh weather exposure. For outdoor architectural applications—window systems, railings, or facade elements—6063's superior corrosion resistance adds long-term durability. Indoor structural applications can safely leverage 6061's strength advantages.
Consider extrudability as well. Complex cross-sections with thin walls, tight radii, or intricate hollow chambers extrude more successfully in 6063. If your custom design pushes geometric boundaries, this alloy's superior flow characteristics reduce manufacturing risks and improve surface quality on challenging features.
Beyond these primary alloys, specialized applications may call for alternatives like 6005 (balancing strength and finish for ladder and platform applications) or 6463 (exceptional brightness for automotive trim and shower enclosures). The right selection ultimately depends on prioritizing the properties that matter most for your specific application—a decision that sets the foundation for everything that follows in the production workflow.
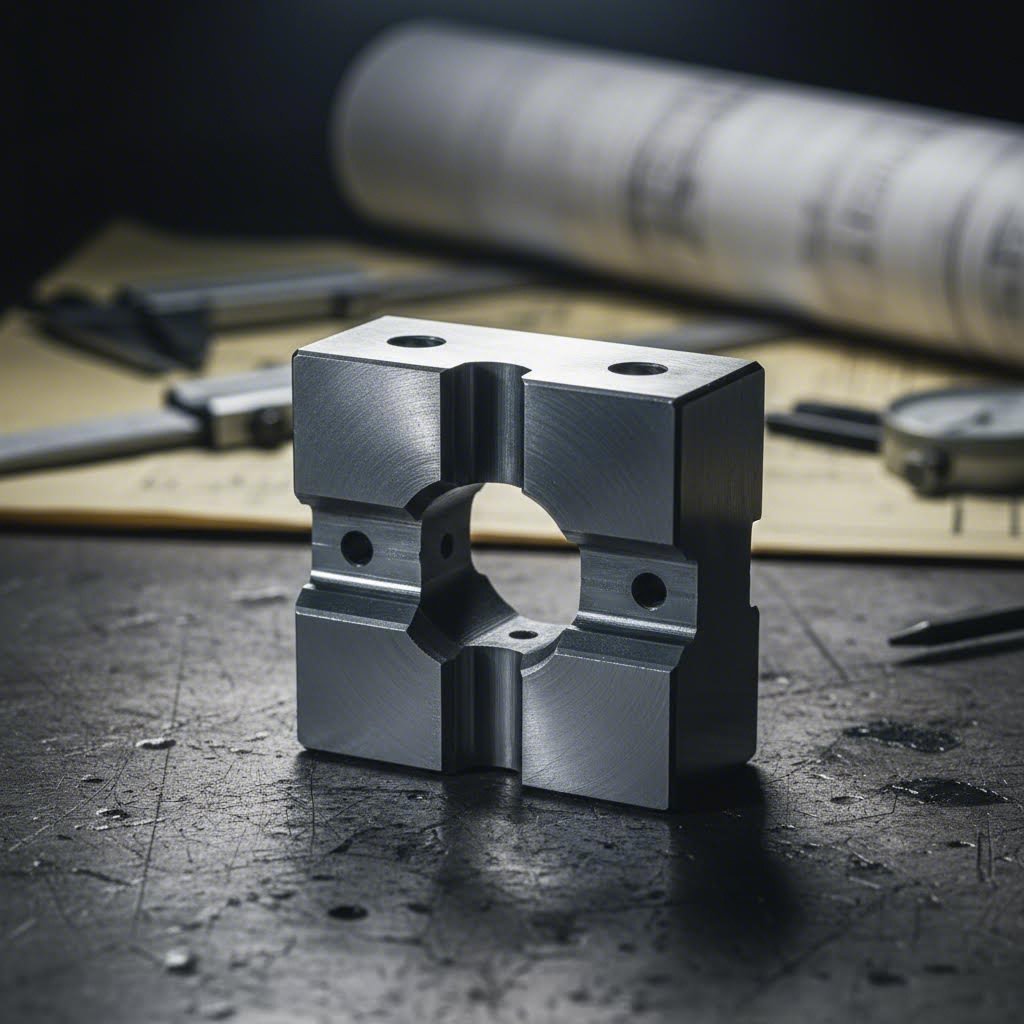
You've selected your alloy—now what? Transforming a concept into finished custom aluminum extrusions requires navigating a structured workflow that many engineers and procurement professionals never see in full detail. Understanding each phase helps you plan timelines, control costs, and avoid costly redesigns midway through production.
The journey from initial idea to delivered parts involves collaboration between your design team and your profile extrusion company at every stage. Let's walk through exactly what happens—and what you need to know—at each critical milestone.
Every custom extrusion project begins with a vision. Maybe you have a napkin sketch, a detailed CAD model, or simply a functional problem that needs solving. Regardless of your starting point, the design development phase establishes the foundation for everything that follows.
Sounds complex? It doesn't have to be. The key is engaging your extrusion partner early—ideally during initial concept development rather than after designs are finalized. Early collaboration prevents the frustrating cycle of designing, discovering manufacturability issues, and redesigning from scratch.
The aluminum extrusion die is where your design becomes reality. This precision-machined steel tool determines everything about your profile's shape, surface quality, and dimensional accuracy.
How aluminium extrusion dies are created: Die manufacturing begins with H13 tool steel—a specialized alloy chosen for its ability to withstand extreme heat and pressure. CNC machining cuts the precise profile opening and bearing surfaces, while wire EDM (electrical discharge machining) creates intricate internal features for hollow profiles. After machining, dies undergo heat treatment to achieve the hardness needed for production use.
Die complexity varies significantly based on profile design:
The aluminium extrusion die design directly impacts metal flow, surface finish, and dimensional consistency. Engineers must balance bearing lengths, flow channels, and pocket depths to ensure aluminum moves evenly through the opening. Unbalanced flow causes profile distortion, surface defects, and dimensional variations—problems that require die modifications to correct.
Typical die life expectations: A well-designed and properly maintained extrusion die can produce impressive quantities before requiring replacement. According to industry analysis, die failures typically result from gradual wear of bearing surfaces, cracking at stress concentration points, or damage from improper handling. Simple solid dies may last for hundreds of thousands of pounds of extruded material, while complex hollow dies experience shorter service lives due to their intricate internal structures.
Die ownership considerations: Who owns the die after production? This question matters more than many buyers realize. Most custom aluminum extrusions projects result in customer-owned tooling—you pay for die development, and the die remains your property (though typically stored at the extruder's facility). This ownership protects your design investment and ensures you can move production if necessary. Clarify ownership terms before committing to any profile custom extrusions project.
Not every shape that looks good on screen extrudes well in practice. Understanding key design constraints helps you create profiles that manufacture efficiently and consistently:
These constraints aren't limitations—they're guidelines that ensure your custom extrusion arrives on spec, on time, and within budget. Experienced extruders will guide you toward designs that balance your functional requirements with manufacturing realities.
Once your die is manufactured and proven, production follows a predictable sequence:
Understanding this workflow empowers you to plan project timelines realistically and communicate effectively with your extrusion partner. With design constraints, die development, and production phases clearly mapped out, the next consideration becomes technical specifications—the precise dimensions, tolerances, and capabilities that transform concepts into manufacturable reality.
When you're ready to specify custom aluminum extrusion profiles, general concepts give way to hard numbers. Engineers and procurement professionals need precise technical parameters—not vague guidelines—to make informed decisions. What press tonnage handles your profile size? What wall thickness can you realistically achieve? How tight can tolerances go before costs escalate?
These questions deserve concrete answers. The specifications you define at this stage directly impact manufacturability, cost, and delivery timelines. Let's dive into the technical details that separate successful extrusion projects from problematic ones.
Dimensional tolerances for extrusion profiles follow industry standards published by the Aluminum Association in ANSI H35.2. However, understanding how these tolerances apply to your specific design requires more nuance than simply referencing a table.
Wall thickness tolerances typically range from ±0.010" to ±0.015" for standard extrusions. According to Silver City Aluminum's design specifications, the larger your dimension, the wider the tolerance range required. A 0.500" outside diameter tube can achieve tighter tolerances (around ±0.003") than a 1.000" tube—a critical consideration when designing mating components.
For aluminum extruded shapes, cross-sectional dimension tolerances depend on the circumscribing circle diameter (CCD)—the smallest circle that completely encloses your profile. Smaller CCDs allow tighter control:
Angular tolerances for corners typically hold ±1° for standard production, though precision applications can achieve ±0.5° with appropriate die engineering. Flatness and twist tolerances become increasingly important for long extrusion profiles—a 20-foot length naturally exhibits more variation than a 6-foot piece cut from the same run.
When specifying aluminum extrusion shapes, identify your critical dimensions explicitly. Extruders can hold tighter tolerances on specific features while allowing standard tolerances elsewhere—a practical approach that balances precision with cost efficiency.
The extrusion press is the muscle behind every profile. Press tonnage determines what size and complexity of extrusion shapes your project can realistically produce.
How press tonnage relates to profile size: Larger profiles require more force to push aluminum through the die opening. A small press in the 600-1,000 ton range handles profiles with CCDs up to approximately 4-5 inches. Medium presses (1,500-3,000 tons) manage profiles up to 8-10 inches. Large-scale operations running 4,000-5,500+ ton presses can produce massive structural shapes with CCDs exceeding 16 inches.
But size isn't the only factor. Profile complexity multiplies the required tonnage. As design guidelines from Ya Ji Aluminum explain, complex profiles with multiple cavities, deep recesses, or irregular geometries demand higher extrusion pressure and slower production speeds. That intricate multi-chamber hollow design might fit within your target CCD yet still require a larger press than a simple solid shape of the same envelope size.
Minimum and maximum profile dimensions:
Profile complexity directly affects manufacturing success. The good news? Strategic design modifications can transform a challenging alum extrusion shapes concept into a smoothly manufacturable reality.
Uniform wall thickness remains the single most important design principle. When aluminum flows through the die, it moves faster through wider sections and slower through thin areas. Unequal flow rates cause twisting, bending, and surface defects in the finished profile. While perfectly uniform walls aren't always possible, keeping adjacent wall thicknesses within a 3:1 ratio—ideally 2:1—minimizes flow-related problems.
Here are key guidelines for optimal aluminum extruded results:
When evaluating your aluminum extrude design, consider whether functional requirements can be met through simpler geometry. According to extrusion design best practices, sometimes two simpler profiles joined mechanically achieve the same result as one complex extrusion—at lower total cost.
The circumscribing circle diameter also affects production economics. Smaller CCDs mean smaller dies, smaller presses, and lower operational costs. If your design can achieve required functionality at a reduced CCD, you'll benefit from improved pricing and broader supplier options.
Armed with these technical specifications, you're prepared to communicate precisely with extrusion suppliers and evaluate their capabilities against your project requirements. But before production begins, there's another critical consideration: what happens to your profiles after they leave the extrusion press?
Your aluminum extrusion emerges from the press with a clean mill finish—but that's rarely the final destination. The real transformation happens during secondary operations, where raw aluminum extrusion parts become finished components ready for assembly and end-use applications. From protective coatings that extend service life to precision machining that creates exact interfaces, these downstream processes often determine whether your project succeeds or falls short.
Understanding which secondary operations your application requires—and when to specify each—helps you plan budgets, timelines, and supplier requirements accurately. Let's explore the complete chain of post-extrusion processes that transform raw profiles into finished extrusion products.
Surface treatments serve two fundamental purposes: protecting the aluminum from environmental degradation and enhancing visual appearance. The right choice depends on your application's exposure conditions, aesthetic requirements, and budget constraints.
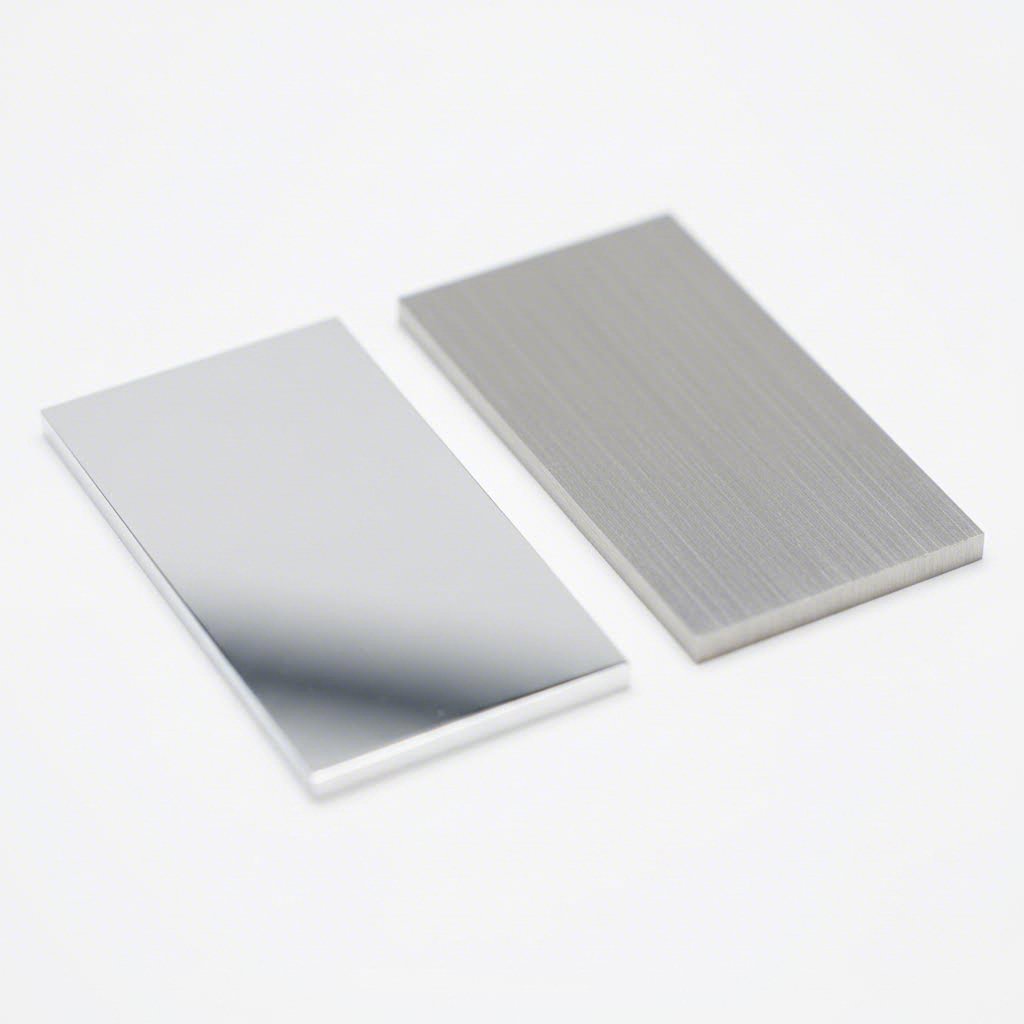
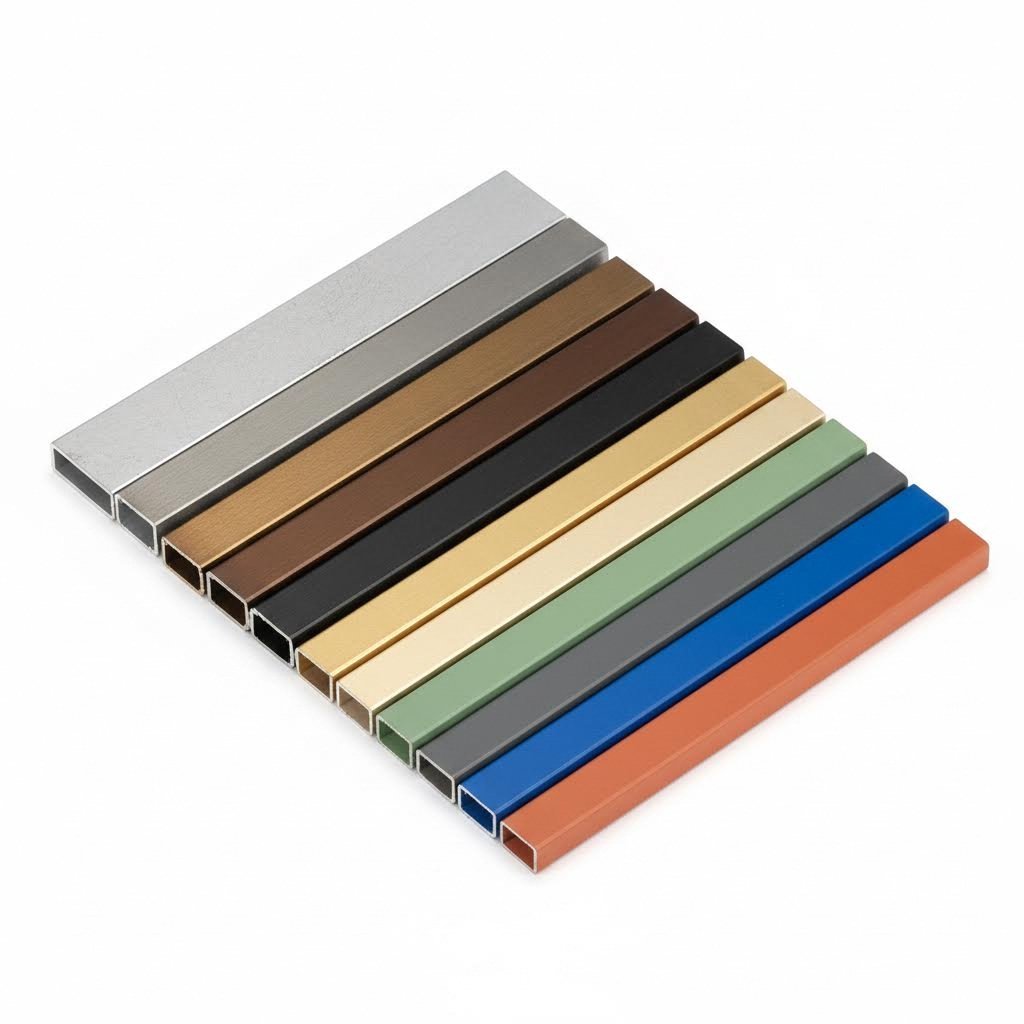
Anodizing remains the most popular surface treatment for aluminum extrusion trim and architectural applications. This electrochemical process converts the aluminum surface into a hard, porous aluminum oxide layer that's integral to the base metal—not a coating that can peel or chip. Clear anodizing preserves aluminum's natural metallic appearance while adding protection. Color anodizing introduces dyes into the porous oxide layer before sealing, creating durable hues ranging from champagne and bronze to rose gold and black.
When should you specify anodizing? Consider it essential for:
Powder coating offers broader color options and thicker protective layers than anodizing. In this process, electrostatically charged powder particles adhere to the grounded aluminum surface, then cure in an oven to form a continuous polymer film. The result? Virtually unlimited color choices, excellent impact resistance, and strong protection against corrosion and chemicals.
PVDF (polyvinylidene fluoride) coatings—often known by brand names like Kynar—provide premium protection for demanding exterior applications. These high-performance fluoropolymer coatings resist fading, chalking, and chemical attack for 20+ years, making them the standard for architectural curtain walls, storefronts, and building facades.
Specialized finishes address unique requirements. Micro-arc oxidation creates exceptionally hard ceramic-like surfaces for high-wear applications. Wood grain sublimation transfers realistic wood patterns onto aluminium extrusion trim for decorative applications that combine aluminum's durability with wood's aesthetics. Brushed, polished, and etched mechanical finishes create distinctive textures before protective clear coats are applied.
| Surface Treatment | Durability | Aesthetic Options | Cost Considerations | Ideal Applications |
|---|---|---|---|---|
| Clear Anodizing | Excellent; 10-20+ years outdoor | Natural metallic appearance; matte or bright | Moderate; varies with coating thickness | Architectural trim, electronics enclosures, decorative parts |
| Color Anodizing | Excellent; maintains appearance under UV | Limited palette (bronze, black, gold tones) | Moderate to high depending on color | Signage, furniture, consumer products, window frames |
| Powder Coating | Very good; 5-15 years outdoor | Unlimited colors; gloss, matte, textured | Economical for large runs; color-matching adds cost | Industrial equipment, outdoor furniture, railings, machinery guards |
| PVDF Coating | Superior; 20+ years with minimal fade | Wide color range; consistent architectural colors | Premium pricing; ideal for high-value projects | Building facades, curtain walls, storefronts, exterior cladding |
| Micro-arc Oxidation | Exceptional hardness and wear resistance | Limited; typically gray or ceramic-like | Higher; specialized process | High-wear components, military, aerospace, industrial machinery |
| Wood Grain Sublimation | Good; protected by clear topcoat | Realistic wood patterns and colors | Moderate to high; pattern-dependent | Architectural accents, pergolas, fencing, interior trim |
Extruded aluminum parts rarely ship as simple cut lengths. Most applications require additional fabrication to create finished, assembly-ready components. The secondary machining chain transforms continuous profiles into precise aluminium extrusion parts ready for integration.
CNC machining opens possibilities that extrusion alone cannot achieve. While the extrusion process creates consistent cross-sections, CNC machining adds features along the profile's length—mounting holes, threaded bosses, pockets, slots, and complex geometries that vary from point to point. Modern CNC machining centers handle cutting, drilling, milling, tapping, and countersinking in automated sequences that maintain tight tolerances across production volumes.
Common secondary operations and their purposes include:
Imagine ordering extruded aluminum trim for a display case. The raw extrusion provides your profile shape, but secondary operations cut pieces to length, miter corners at precise angles, drill mounting holes, and apply the anodized finish—delivering components ready for final assembly rather than raw material requiring additional processing at your facility.
The capability of your extrusion supplier to perform these operations in-house significantly affects lead times and costs. Partners equipped with comprehensive CNC machining centers, surface treatment lines, and assembly capabilities deliver finished extruded aluminum parts rather than semi-processed profiles requiring additional vendor coordination. For complex projects, working with a supplier like Shengxin Aluminium—with 30+ years of experience, 35 extrusion presses, dedicated CNC machining centers, and extensive surface treatment options including anodizing, powder coating, PVDF, and micro-arc oxidation—streamlines your supply chain from die development through finished part delivery.
With surface treatments and fabrication capabilities defined, understanding what drives costs becomes the next essential consideration for project planning and budgeting.
What does custom aluminum extrusion actually cost? It's the question everyone asks—and the one most suppliers avoid answering directly. The reality is that aluminum extrusion cost depends on multiple interconnected variables, and understanding these drivers empowers you to make smarter procurement decisions and optimize your project budget.
Unlike commodity products with fixed price lists, custom aluminium extrusion pricing reflects the unique combination of tooling investment, material selection, production volume, and finishing requirements your project demands. Let's break down exactly what influences your per-piece pricing.
When you request a quote for custom aluminum extrusion profiles, suppliers evaluate several cost components that combine to determine your final price. Here are the primary drivers:
Think of it this way: ordering 500 feet of a simple rectangular tube in 6063 with mill finish represents the lowest-cost scenario. Add a complex hollow cross-section, switch to 6061 alloy, specify precision tolerances, and require anodized finishing—each addition layers onto your base cost.
Aluminum extrusion tooling represents your most significant upfront investment. Die costs for custom aluminum products typically range from a few hundred dollars for simple solid shapes to several thousand dollars for complex hollow profiles with tight tolerances.
Here's what affects die pricing:
Smart buyers amortize die costs over expected production volume. If your aluminum extrusion dies cost $2,000 and you plan to order 10,000 pieces over the product lifecycle, you're adding just $0.20 per piece for tooling. Order only 500 pieces? That same die adds $4.00 per unit—a twenty-fold difference.
When does custom extrusion become cost-effective? Generally, custom aluminum extrusion beats machining from solid stock when order quantities exceed a few hundred pieces, depending on profile complexity. Extrusion's efficiency shines as volumes grow—the process produces finished cross-sections in one pass rather than removing material through multiple machining operations. For production runs in the thousands, custom extrusion delivers substantial savings compared to alternative manufacturing methods.
Minimum order quantities typically start around 300-500 pounds for most extruders, though some accommodate smaller prototype runs at premium pricing. Production economics favor larger orders, where press setup time and die installation costs spread across greater output volumes.
With cost factors clearly understood, planning realistic production timelines becomes your next priority—because knowing what you'll pay matters little if you can't predict when you'll receive your parts.
You've finalized your design, selected your alloy, and approved the budget—now comes the question that keeps procurement professionals up at night: when will parts actually arrive? Unlike stock aluminum extrusions that ship from inventory within days, custom extrusions require manufacturing time that many buyers underestimate during project planning.
Understanding realistic timeline expectations prevents schedule conflicts and helps you coordinate custom aluminum extrusion profiles with downstream assembly operations. Let's map out exactly what to expect at each production phase.
Every custom extrusions project moves through distinct phases, each with its own timeline considerations. Here's what typical schedules look like from design approval to delivery:
Total timeline for new custom projects typically ranges from 6-12 weeks depending on complexity. Reorders using existing dies skip the tooling phases entirely, reducing lead times to 3-5 weeks for production and finishing.
Why do some projects finish faster than others? Several variables influence your actual delivery date beyond baseline expectations.
Complexity impacts every phase. Small aluminum extrusions with simple solid cross-sections move through die manufacturing quickly and extrude at faster speeds. Intricate hollow profiles with tight tolerances require extended die fabrication, slower extrusion rates, and more careful quality verification—potentially adding 2-3 weeks to your schedule.
Order size affects production scheduling. Aluminum extrusion companies batch similar alloys and profile sizes to maximize press efficiency. Large orders receive dedicated press time, while smaller runs may wait for scheduling windows that minimize changeover costs. Planning procurement around supplier production cycles can shave days from delivery timelines.
Finishing requirements extend timelines. Mill finish profiles ship fastest. Anodizing adds 5-10 days for processing and curing. Complex powder coating specifications with custom color matching may require 2-3 weeks. PVDF architectural coatings demand additional lead time for specialized application processes.
Tips for expediting your project:
Effective procurement planning accounts for these variables realistically. Build buffer time into project schedules—rushing custom extrusion work rarely ends well, while adequate lead time ensures quality results delivered when you need them. With timeline expectations set, the final consideration becomes matching your project requirements to the right applications and supplier capabilities.
Where do custom aluminum extrusion profiles actually end up? The answer spans an impressive range—from the sleek window frames defining modern skyscrapers to the rugged structural framing inside manufacturing equipment. This versatility explains why aluminum extrusions have become the go-to solution for designers and engineers across vastly different industries.
Understanding how application requirements shape profile design helps you specify the right characteristics for your project. An architect prioritizing visual refinement approaches custom extrusion differently than a mechanical engineer focused on thermal performance or structural capacity. Let's explore how both worlds leverage extruded aluminum shapes to solve distinct challenges.
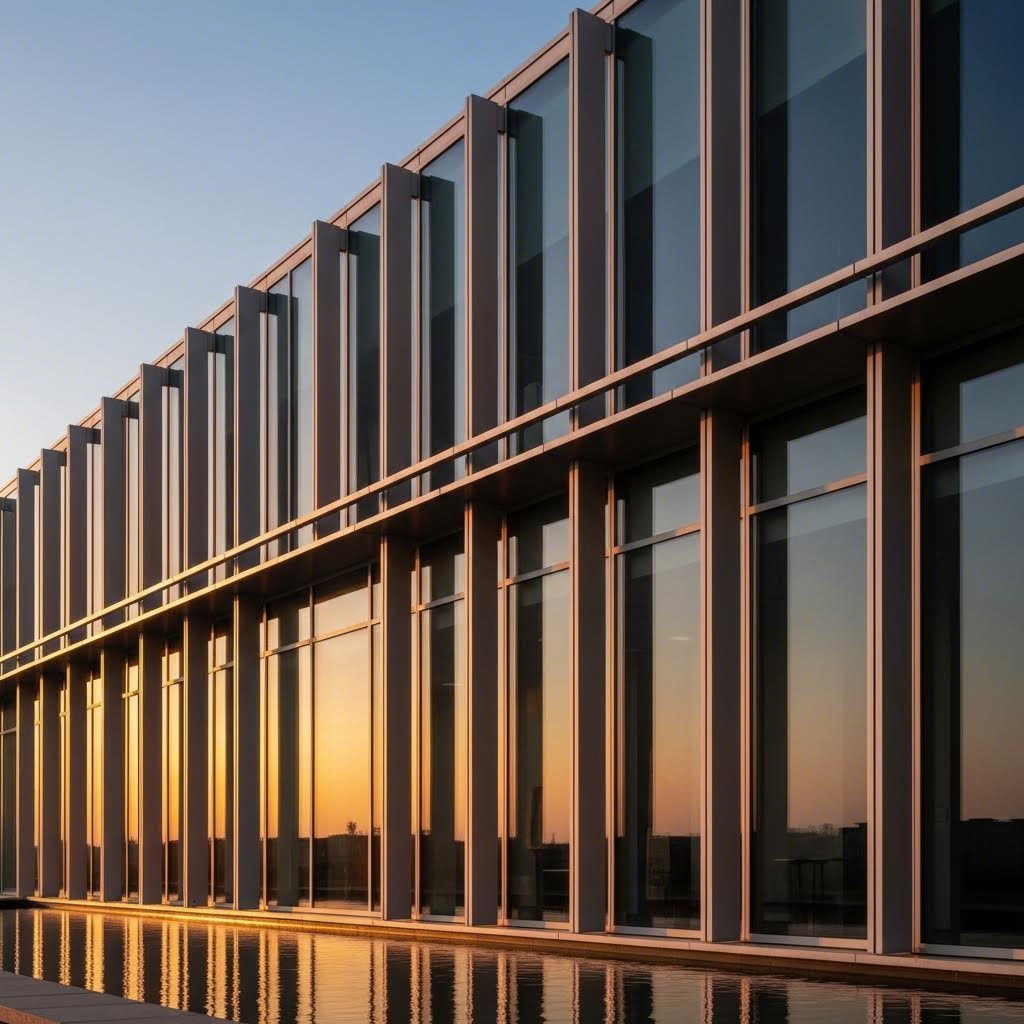
Walk through any contemporary building and you're surrounded by aluminum profile extrusion applications—often without realizing it. The architectural sector relies heavily on custom aluminum profiles because they deliver the perfect combination of design flexibility, durability, and aesthetic consistency that building projects demand.
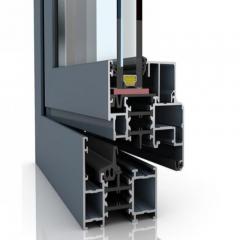
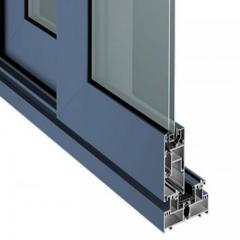
Window and door systems represent the largest architectural application for fabricated aluminum profiles. Modern thermally broken window frames use complex multi-chamber extrusions that separate interior and exterior aluminum sections with insulating polymer barriers. These designs require precise dimensional control for weatherseal integration and hardware compatibility, plus excellent surface finish quality for visible applications.
Curtain wall systems showcase aluminum's structural and aesthetic capabilities at building scale. The mullions, transoms, and pressure plates that comprise curtain wall frameworks are custom-designed extrusions engineered for specific structural loads, thermal performance, and drainage requirements. PVDF-coated finishes ensure these exposed profiles maintain their appearance for decades despite constant weather exposure.
Additional architectural applications include:
Architectural projects prioritize surface finish quality above most other considerations. Profiles destined for visible applications require 6063 alloy's superior anodizing response, tight control over surface defects, and consistent color matching across production lots. Design requirements emphasize clean sight lines, concealed fastening methods, and integration with glazing gaskets and weatherseals.
Bespoke aluminium extrusion designs allow architects to create distinctive building identities impossible with standard profiles. A custom mullion cap, proprietary trim shape, or signature decorative element becomes part of the project's visual language—differentiation that standard catalog shapes simply cannot provide.
Step inside a manufacturing facility and the priorities shift dramatically. Here, aluminum extrusions prove their worth through structural performance, thermal management, and functional precision rather than visual appeal. Industrial applications push profile design toward optimization for specific engineering requirements.
Structural framing systems dominate industrial extrusion applications. T-slot aluminum framing—those modular profiles with standardized slot geometries—builds everything from machine guards and workstations to conveyor structures and cleanroom enclosures. Custom variations optimize these systems for specific load requirements, integration points, or space constraints that standard T-slot catalogs cannot address.
Heat sink profiles demonstrate aluminum's exceptional thermal conductivity. LED lighting fixtures, power electronics, motor drives, and computing equipment all rely on extruded heat sinks to dissipate thermal energy. These profiles feature precisely calculated fin geometries—thin, closely spaced fins maximize surface area for convective cooling while maintaining structural integrity during handling and assembly.
Industrial aluminum extrusions serve diverse sectors:
Industrial applications typically favor 6061 alloy when structural demands outweigh finishing concerns. The higher tensile strength supports load-bearing applications, while machinability matters more than anodizing response when profiles require extensive secondary operations.
The contrast between architectural and industrial profile design reveals how application context shapes every specification decision.
Aesthetic-focused architectural projects demand:
Performance-driven industrial applications prioritize:
Consider a practical example: unique extrusions designed for an LED light fixture. The architectural version emphasizes smooth visible surfaces, integrated lens retention features, and a profile shape contributing to the luminaire's design aesthetic. The industrial version—perhaps for warehouse high-bay lighting—prioritizes heat sink fin density, mounting hole provisions, and rugged construction over visual refinement.
Both applications leverage aluminum extrusion's fundamental advantages: complex geometries in a single manufacturing step, excellent strength-to-weight ratios, inherent corrosion resistance, and cost-effective production at volume. The difference lies in which properties receive design emphasis and how trade-offs between competing requirements get resolved.
Whether your project leans architectural or industrial—or bridges both worlds—success depends on partnering with an extrusion supplier whose capabilities align with your specific requirements.
You've designed your profile, specified your alloy, and mapped out your production requirements—now comes perhaps the most consequential decision of all: choosing who will actually manufacture your custom aluminum extrusion profiles. The wrong partner can turn a well-planned project into a frustrating cycle of delays, quality issues, and cost overruns. The right partner becomes a long-term asset that elevates your product and streamlines your supply chain.
How do you distinguish between custom aluminum extruders that merely claim capability and those that consistently deliver? The answer lies in systematic evaluation—examining technical capacity, quality systems, production resources, and support infrastructure before committing to any supplier relationship.
When researching custom aluminum extrusions suppliers, resist the temptation to focus solely on quoted prices. Low bids from underqualified suppliers often lead to hidden costs through rejected parts, delayed shipments, and project restarts. Instead, evaluate potential partners across multiple capability dimensions:
Consider what comprehensive capability looks like in practice. A profile custom extrusion company like Shengxin Aluminium exemplifies the infrastructure serious buyers should expect: 30+ years of industry experience, 35 extrusion presses spanning 600T to 5500T capacity, dedicated CNC machining centers for precision secondary operations, and extensive surface treatment options including anodizing, powder coating, PVDF, and micro-arc oxidation. This breadth of capability means your custom extruded aluminum projects—from die development through finished part delivery—can be managed through a single accountable partner.
Smart procurement goes beyond reviewing capability brochures. Direct conversations with potential custom extrusion aluminum suppliers reveal whether their claims match operational reality. Before committing, ask these essential questions:
When soliciting quotes from multiple suppliers, provide identical specifications to ensure apples-to-apples comparison. Your RFQ package should include detailed drawings with dimensions and tolerances, alloy specification, temper requirements, surface finish expectations, estimated annual volume, and secondary operation requirements.
Evaluate quotes beyond unit pricing. Consider:
Before production commitment, always request sample extrusions for physical evaluation. Check dimensional accuracy against your specifications, examine surface quality for defects or inconsistencies, verify mechanical properties if critical to your application, and test fit with mating components. Samples reveal manufacturing capability more reliably than any sales presentation.
Clear quality agreements prevent disputes and ensure consistent results across production runs. Work with your chosen supplier to establish:
The effort invested in thorough supplier evaluation pays dividends throughout your project lifecycle. A qualified partner—one with the technical depth, production resources, and quality commitment your application demands—transforms custom aluminum extrusion from a procurement challenge into a competitive advantage. Take time to evaluate thoroughly, ask probing questions, and verify capabilities through samples before committing. Your project's success depends on it.
Standard aluminum extrusion profiles include common shapes like angles, channels, and tubes available from stock for general applications. Custom profiles are designed specifically for your project, allowing you to integrate multiple functions into a single piece, optimize weight distribution, achieve exact dimensional requirements, and create unique aesthetics. Manufacturers choose custom extrusions when standard shapes cannot deliver required performance, integration, or efficiency—such as LED housings that incorporate heat sinks, mounting channels, and decorative trim in one seamless profile.
Custom aluminum extrusion costs depend on several interconnected factors: die complexity (simple solid profiles cost less than multi-cavity hollow shapes), alloy selection (6061 costs more than 6063), order volume (higher quantities reduce per-unit pricing), profile size, finishing requirements, secondary operations, and tolerance specifications. Die tooling represents the largest upfront investment, ranging from a few hundred to several thousand dollars. Generally, custom extrusion becomes cost-effective compared to machining from solid stock when order quantities exceed a few hundred pieces.
The 6000 series alloys dominate custom extrusions, with 6063 and 6061 being the most common choices. Aluminum 6063 (the 'architect's alloy') offers superior surface finish quality and excellent corrosion resistance, making it ideal for anodized architectural applications like window frames and decorative trim. Aluminum 6061 (the 'engineer's alloy') provides higher tensile strength (45,000 psi vs 30,000 psi) and better machinability, suited for structural components, heat sinks, and machinery parts where strength outweighs finishing concerns.
New custom extrusion projects typically require 6-12 weeks from design approval to delivery. This includes die design and engineering (1-2 weeks), die manufacturing (2-4 weeks), die trial and first article production (3-5 days), sample approval (1-2 weeks), production extrusion (1-3 weeks), secondary operations and finishing (1-3 weeks), and quality inspection with shipping (3-7 days). Reorders using existing dies skip tooling phases, reducing lead times to 3-5 weeks. Complex profiles, large orders, and specialized finishes extend timelines.
Evaluate potential suppliers across multiple dimensions: press capacity range suited to your profile size, die engineering expertise with similar profile complexity, in-house secondary operations (CNC machining, anodizing, powder coating), quality certifications like ISO 9001, production capacity for your volume requirements, and responsive technical support. Partners like Shengxin Aluminium with 30+ years experience, 35 extrusion presses (600T-5500T), dedicated CNC centers, and comprehensive surface treatments can manage projects from die development through finished part delivery under one roof.


 Інтернет-сервіс
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 Українська
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Việt