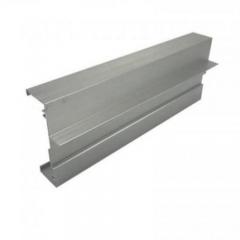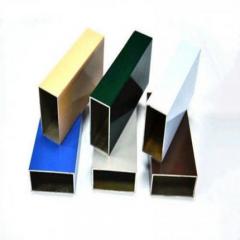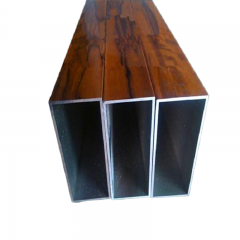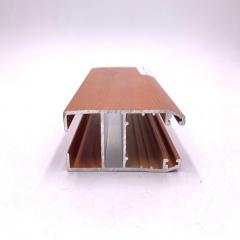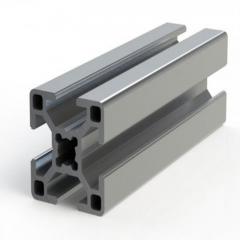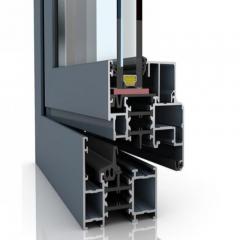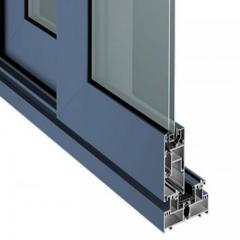
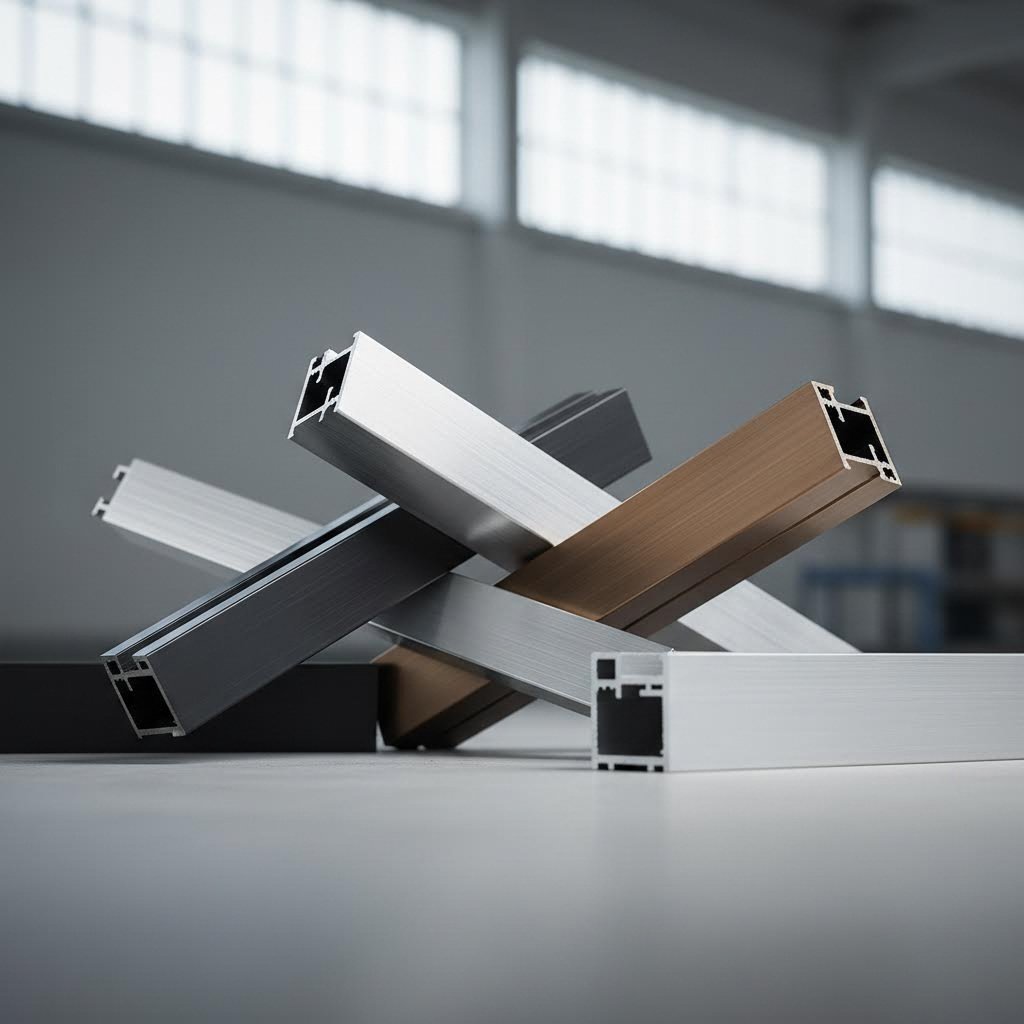
Anodized aluminum extrusion is an aluminum profile that has undergone an electrochemical process to create a durable, protective oxide layer that becomes permanently integrated into the metal's surface. Unlike paint or powder coating that sits on top of aluminum, this oxide layer grows directly from the base metal itself, creating protection that cannot chip, peel, or flake away. This fundamental difference makes anodized aluminum extrusions the preferred choice for applications demanding long-term durability, from architectural facades to precision industrial components.
When you examine an anodized extruded aluminum profile, you're looking at a material that has been chemically transformed rather than simply coated. This transformation delivers enhanced corrosion resistance, improved hardness, and superior wear resistance that lasts for decades. But how exactly does aluminum undergo this remarkable change?
Imagine submerging an aluminum profile into an electrolytic bath and watching chemistry reshape its very surface. That's essentially what happens during anodizing. The process begins with thorough cleaning and etching of the aluminum extrusion to remove any dirt, oils, or naturally occurring oxide. Technicians then place the cleaned profile into an acid bath, typically containing sulfuric acid, and apply an electrical current.
Here's where the science gets interesting. When electricity flows through the solution, oxygen ions are released and migrate toward the aluminum surface. These ions combine with the aluminum atoms to form aluminum oxide, a crystalline structure that's incredibly hard and stable. According to Xometry, you can control the thickness of this oxide layer by adjusting the current density, immersion time, temperature, and electrolyte concentration.
The resulting oxide layer isn't just sitting on the surface. It actually grows both inward and outward from the original aluminum surface, becoming chemically bonded to the base metal. This creates a porous structure with tiny cylindrical channels running perpendicular to the surface, perfect for accepting dyes or sealants that further enhance the finish.
You might wonder why anodizing matters when you could simply paint or powder coat aluminum. The distinction is critical for performance and longevity.
The anodized oxide layer is not applied on top of the aluminum—it is integral to it. This layer grows from the aluminum itself, making it impossible to chip, peel, or separate from the base metal.
Surface coatings like paint or powder coating create a mechanical bond with aluminum. They adhere to the surface but remain separate materials. Over time, these coatings can scratch through to the base metal, peel at edges, or degrade under UV exposure. In contrast, anodized aluminum extrusions offer protection that cannot be compromised in these ways because the protective layer is the aluminum, transformed at the molecular level.
This electrochemical transformation delivers several practical advantages:
According to industry sources, an anodized coating can last between 10 and 20 years depending on the application, coating thickness, and whether proper sealing was performed. That longevity, combined with the integrated nature of the protection, explains why architects, engineers, and product designers consistently specify anodized aluminum extrusions for demanding applications.
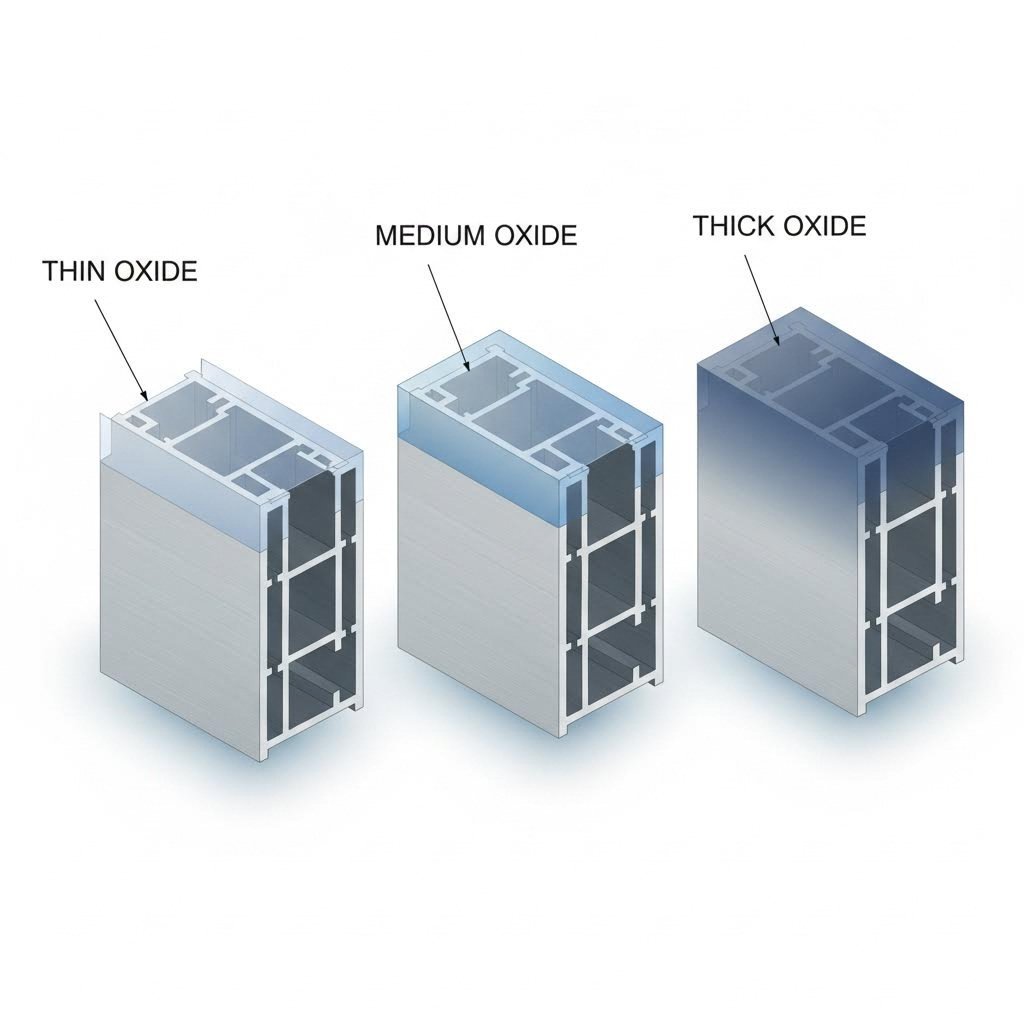
Not all anodizing is created equal. When specifying anodized aluminum extrusion for your project, understanding the differences between Type I, Type II, and Type III anodizing can mean the difference between a part that performs flawlessly for decades and one that fails prematurely. Each type uses a distinct process, produces different oxide layer thicknesses, and serves specific applications. Let's break down what sets them apart.
The classification system follows military specification MIL-A-8625, which has become the worldwide standard for commercially anodized aluminum. This specification defines each type based on the electrolyte used, the resulting coating thickness, and the intended performance characteristics.
| Process Type | Oxide Thickness Range | Hardness Rating | Corrosion Resistance | Typical Applications | Cost Level |
|---|---|---|---|---|---|
| Type I (Chromic Acid) | 0.5 - 2.5 μm (0.00002" - 0.0001") | Moderate | Excellent | Aerospace components, paint base, tight-tolerance parts | High |
| Type II (Sulfuric Acid) | 1.8 - 25 μm (0.00007" - 0.001") | Good | Very Good | Architectural, decorative, general industrial, black aluminum extrusion | Moderate |
| Type III (Hardcoat) | 25 - 150 μm (0.001" - 0.006") | 65-70 Rockwell C (850-900 DPH) | Superior | Wear components, large aluminium extrusions for heavy industry, military equipment | High |
When dimensional precision matters most, Type I anodizing stands apart. This process uses a chromic acid electrolyte to produce the thinnest protective layer of all three types, typically measuring less than 2.5 microns. Why does this matter? For aerospace components and precision assemblies, even a few extra microns on a part can cause fit problems in complex assemblies.
According to industry experts, Type I anodizing offers a significant advantage: it has less impact on aluminum's fatigue strength compared to Type II. The process is also self-limiting, meaning if any chromic acid solution becomes trapped in cracks or seams, it won't corrode the underlying aluminum like sulfuric acid might.
You'll commonly find Type I anodizing specified for:
However, Type I has limitations worth considering. The resulting finish is a dull gray color that cannot be dyed due to the thin, non-porous nature of the oxide layer. Additionally, chromic acid is classified as a hazardous material, making this process more expensive and less widely available as environmental regulations tighten.
Here's where things get interesting for most applications. Type II and Type III anodizing both use sulfuric acid baths, but the similarities largely end there. The processing parameters, resulting properties, and ideal applications differ dramatically.
Type II sulfuric acid anodizing represents the most commonly specified finish for anodized aluminum extrusions. This process produces coatings between 1.8 and 25 microns thick, creating a porous structure that accepts dyes beautifully. Want black extruded aluminum for your project? Type II is your answer. Need clear anodized aluminium that maintains aluminum's natural metallic appearance? Type II delivers.
The Type II process works at moderate temperatures and voltages, making it cost-effective for high-volume production. After anodizing, the porous oxide layer can be dyed in virtually any color before sealing locks in both the color and corrosion protection. This combination of durability, aesthetic versatility, and reasonable cost explains why Type II dominates architectural and consumer product applications.
Type III hardcoat anodizing takes an entirely different approach. The process runs in a refrigerated tank near the freezing point of water and uses higher voltages to build substantially thicker oxide layers. According to Anodize Inc., Type III produces coatings exceeding 25 microns, with thicknesses up to 150 microns possible for extreme applications.
The performance difference is striking. Type III hardcoat achieves hardness ratings of 65 to 70 Rockwell C, which translates to approximately 850-900 DPH (Diamond Pyramid Hardness). This makes the anodized surface harder than tool steel. For large aluminium extrusions used in heavy industrial equipment, mining operations, or military vehicles, this exceptional hardness translates directly to extended service life.
Critical differences to remember when choosing between Type II and Type III:
One important consideration: you cannot layer these processes. You cannot apply hardcoat over existing anodizing, add thickness to an existing coating, or build up Type III over Type II. The anodizing specification must be determined upfront based on your application's requirements.
Understanding these distinctions empowers you to specify exactly what your project needs. But selecting the right anodizing type is just one piece of the puzzle. The color options available, and how to achieve consistent results across production runs, present their own set of considerations worth exploring.
Selecting the right anodizing type is only half the equation. The color you choose transforms how your anodized aluminum extrusion looks, performs, and integrates with your overall design. From the clean metallic look of clear anodizing to the rich warmth of bronze anodized aluminum and the sleek sophistication of black aluminium extrusion, your options span an impressive spectrum. But here's what most suppliers won't tell you: achieving the exact color you envision depends on factors that go far beyond picking a shade from a catalog.
Understanding how color works in anodizing requires thinking differently than you would about paint. According to industry experts, anodizing colors are subtractive rather than additive. The formed oxide film transmits light to the aluminum base, which reflects it back through the film. This transforms the anodized layer into a filter rather than a simple reflector, which is crucial for understanding why color matching can be challenging.
When you want aluminum to look like aluminum, clear anodizing delivers. This finish creates a transparent, protective layer that preserves the metal's natural appearance while dramatically improving its durability. The result maintains that distinctive metallic sheen architects and designers often seek for modern applications.
Here are the most common color options available for anodized aluminum extrusions:
Clear anodizing isn't truly colorless. According to technical resources, pure aluminum grades like 1050 and 1100 typically appear silver-white when anodized in sulfuric acid baths. However, add copper to the alloy, and you'll notice a shift toward gray or even reddish undertones. This relationship between alloy composition and final appearance is something every buyer should understand before specifying a finish.
Here's a reality that surprises many first-time buyers: you cannot simply pick any color and expect perfect results on any aluminum alloy. The base metal's composition fundamentally influences what's achievable.
The aluminum oxide layer formed during anodizing incorporates alloying elements from the base metal. Copper, zinc, magnesium, and silicon all embed themselves in the oxide coating as it grows, changing its optical properties and how it accepts dyes. According to Precision Coating, alloys like 2024 (high copper content) and 7075 (high zinc content) produce a dark gray color after anodizing, making lighter color matching extremely difficult.
For the best color results, consider these alloy guidelines:
Imagine ordering 500 bronze anodized aluminum extrusions, only to find noticeable shade variations between the first and last batches. This scenario plays out more often than suppliers like to admit, but understanding the variables helps you prevent it.
Color consistency challenges stem from multiple sources. According to Zintilon, factors including oxide layer thickness, immersion time, dye concentration, and power source rating all influence color intensity. Even the quality and concentration of dyes across different batches can introduce variation. Layering effects between dye applications add another variable, as colors can shift between layers.
To minimize color variation in your orders, specify these parameters clearly:
There's another phenomenon worth knowing about: color flip. According to technical sources, the reflective properties of aluminum are influenced by the metal's crystalline structure. Colors may appear to match from one viewing angle, but shift when the angle changes. This effect is particularly noticeable with metallic finishes and can complicate approval processes if you're comparing samples under different lighting conditions.
When dealing with large production loads, expect some coating thickness range across parts. The current density during anodizing creates a window effect, with the greatest intensity at edges. This naturally results in slight color variation across a batch. Working with your anodizing partner to establish acceptable ranges before production begins saves headaches during quality inspection.
Understanding color options and consistency challenges prepares you to specify exactly what you need. But achieving a flawless finish depends on more than color selection. The physical design of your extrusion profile plays an equally important role in determining whether your anodized parts meet expectations.
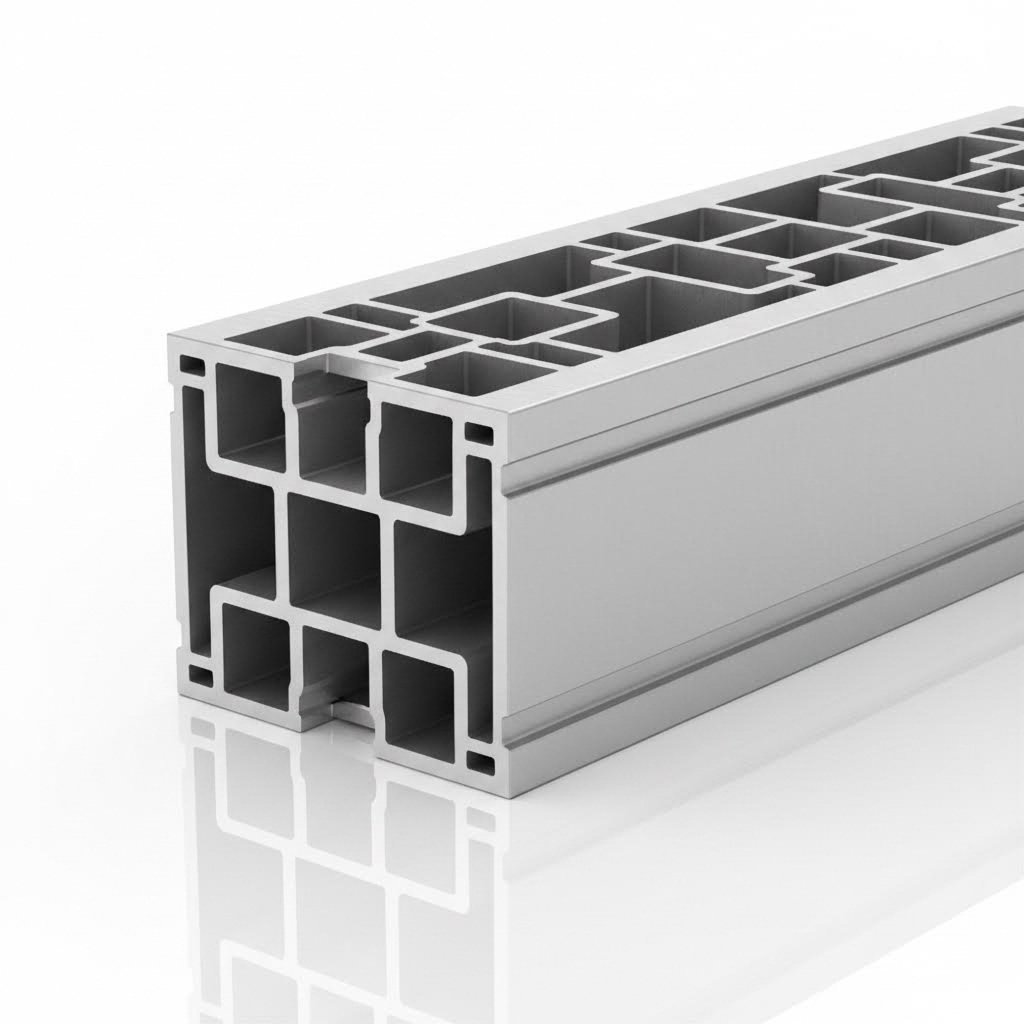
Here's something most suppliers won't discuss upfront: the shape of your extruded aluminum profile directly influences how well the anodizing process works. You could specify the perfect anodizing type, select an ideal color, and still end up with inconsistent results if the profile geometry wasn't designed with anodizing in mind. Whether you're working with a t slot aluminum profile for industrial framing or a custom channel for architectural trim, understanding this relationship saves you from costly rework and rejected parts.
Think about what happens during anodizing. Electrical current flows through the aluminum while it's submerged in an acid bath, and oxygen ions migrate toward the surface to form the oxide layer. But current doesn't distribute evenly across complex shapes. It concentrates at edges and external corners while struggling to reach deep recesses and internal angles. This physical reality means your profile design directly determines coating uniformity.
When current flows through an aluminum extrusion during anodizing, it follows the path of least resistance. External corners and edges receive higher current density, resulting in thicker oxide buildup. Internal corners, deep channels, and recessed areas receive less current, producing thinner coatings. This phenomenon creates real-world performance differences across a single part.
According to Silver City Aluminum, wall thickness uniformity ranks among the most overlooked design considerations. Shapes with uniform wall thickness extrude more easily because aluminum flows through the die at an even rate. But this principle extends to anodizing as well. When walls vary significantly in thickness, the thicker sections absorb more current during processing, leading to uneven oxide formation.
Consider an aluminum t rail with thick base sections and thin flanges. During anodizing, the base may develop a robust oxide layer while the thin flanges receive marginal coating. The visual result? Color variations between thick and thin sections that become especially noticeable with darker dyes like black or bronze.
Sharp corners present another challenge worth understanding. According to industry guidelines, extrusion dies cannot produce corners with radii less than 0.005 inches. The wire EDM cutting process used to create dies inherently produces rounded corners. But beyond manufacturing limitations, sharp internal corners create current shadows during anodizing, leaving these areas vulnerable to thin coating and reduced corrosion protection.
Complex profiles like t slot aluminum profiles, multi-channel extrusions, and intricate architectural shapes require thoughtful design to anodize successfully. The good news? Most anodizing challenges can be prevented with proper planning during the design phase.
Follow these design best practices for optimal anodizing results:
For extruded aluminum profiles with T-slots, the slot geometry deserves special attention. The internal corners where the slot meets the main body often receive less current during anodizing. If your application exposes these areas to corrosive environments, discuss coating thickness requirements for internal surfaces with your anodizing provider.
Here's a critical detail that catches many engineers off guard: anodizing changes your part dimensions. The oxide layer doesn't simply sit on top of the original surface. According to Sanford Process Corporation's technical guidelines, approximately half of the coating thickness penetrates into the aluminum while the other half builds outward from the original surface.
For Type III hardcoat with a typical thickness of 0.002 inches, this means each surface grows outward by approximately 0.001 inches. On a hole or bore, this translates to 0.002 inches reduction in diameter. On external dimensions, expect 0.002 inches growth per surface, or 0.004 inches on overall width.
But dimensional changes don't stop at the anodizing step. Pre-treatment etching removes aluminum before anodizing begins. According to technical documentation, standard etching removes 0.0001 to 0.0006 inches per surface in typical 1 to 4 minute processes. Heavy etching for mill-finish extrusions can remove up to 0.0015 inches on diameter. Chemical brightening adds another variable, potentially removing 0.0002 inches per surface.
The practical takeaway? If you're manufacturing tight-tolerance parts, communicate with your anodizing provider before production begins. Specify your final dimensional requirements and work backward to determine appropriate machined dimensions. Leaving holes undersized to account for expected buildup, while neglecting to factor in material removal during pre-treatment, leads to out-of-tolerance parts that cannot be salvaged.
When cosmetic appearance and tight tolerances must coexist, compromises become necessary. As Sanford Process notes in their guidelines, "cosmetics and tight tolerances are at odds" when working with as-extruded or sheet material requiring heavy etching for visual uniformity. Defining which requirement takes priority before manufacturing begins prevents disputes during quality inspection.
With profile design optimized for anodizing success, the next critical factor is understanding the pre-treatment and sealing processes that transform raw extrusions into finished products ready for demanding applications.
You've selected the right anodizing type, chosen your color, and optimized your profile design. But here's what separates a mediocre finish from an exceptional one: the steps that happen before and after the aluminum ever enters the anodizing tank. According to anodizing experts, the complete process consists of seven distinct steps excluding rinsing, and skipping or rushing any of them invites defects that compromise both appearance and performance.
Think of pre-treatment as preparing a canvas before painting. No matter how skilled the artist, a dirty or uneven canvas produces disappointing results. Similarly, post-treatment sealing acts as the protective varnish that locks in your investment. Understanding these processes helps you communicate effectively with suppliers and recognize quality work when you see it.
Before anodizing can begin, the aluminum surface must be meticulously prepared. Any contamination, oxidation, or surface irregularity that exists before treatment will show up in the final product, often amplified. Here's the sequence that professional anodizers follow:
Each pre-treatment step builds on the previous one. Rush the cleaning, and grease deposits will create uneven etching. Skip proper rinsing after etching, and alkaline residue will contaminate the desmutting bath. The cascade effect means that quality problems in early steps multiply as the process continues.
After anodizing and any coloring steps, the aluminum surface features a porous oxide structure resembling a honeycomb at the microscopic level. This porosity is useful for absorbing dyes, but it creates a vulnerability. According to technical sources, an unsealed surface readily absorbs water and aggressive substances that can diminish corrosion protection and fade colors over time.
Sealing closes these pores, and according to Products Finishing, it's considered the most important step in the entire anodizing process. How you seal determines how the anodic oxide performs in its end-use environment. Several sealing methods exist, each with distinct advantages:
Understanding what can go wrong helps you specify requirements that prevent problems. Most anodizing defects trace back to preparation or sealing failures rather than the anodizing step itself.
Color variation often stems from inconsistent oxide layer thickness, which results from uneven current distribution during anodizing. But it can also originate earlier in the process. Inadequate cleaning leaves organic residues that interfere with oxide formation. Inconsistent etching creates surface variations that affect how uniformly the oxide layer develops. These preparation defects become visible only after dyeing, when it's too late to correct them.
Poor sealing creates long-term problems that may not appear immediately. According to technical resources, inadequate sealing leaves the surface open to chemical and physical damage. Colors fade as environmental contaminants penetrate the porous structure. Corrosion protection degrades over time. Parts that looked perfect at delivery may fail prematurely in service.
How do you know whether your anodized parts meet specifications? Several standardized tests verify coating quality:
Open communication between you and your anodizing provider prevents most quality issues. According to industry guidance, customers should provide information about the alloy, metallurgical history, and intended end-use environment. This information helps anodizers select appropriate pre-treatment chemistry, anodizing parameters, and sealing methods tailored to your specific requirements.
With pre-treatment and sealing processes understood, the next step is matching all these specifications to your actual application requirements. Different industries and use cases demand different combinations of anodizing type, color, and processing parameters.
You've mastered the fundamentals of anodizing types, colors, and processing. Now comes the practical question every buyer faces: which specifications actually work for your specific project? Whether you're designing window frames for a coastal building, assembling a t aluminum framing system for a production line, or manufacturing precision components for aerospace, the right anodizing specification transforms a good design into a lasting solution.
The challenge? Different applications demand different performance characteristics. A decorative interior trim doesn't need the same wear resistance as a conveyor system component. An architectural curtain wall faces environmental stresses that electronics enclosures never encounter. Matching your application to the correct anodizing specification prevents both over-engineering (wasting money) and under-engineering (risking premature failure).
| Application Category | Recommended Anodizing Type | Minimum Oxide Thickness | Key Performance Requirements |
|---|---|---|---|
| Architectural Exteriors (curtain walls, storefronts) | Type II, Class I or II | 18 μm (0.0007") | UV stability, corrosion resistance, color consistency |
| Interior Decorative (trim, fixtures) | Type II, Class I | 10 μm (0.0004") | Aesthetic appearance, scratch resistance |
| T-Slot Framing Systems | Type II or Type III | 15-25 μm (0.0006"-0.001") | Wear resistance, dimensional stability |
| Machinery Components | Type III | 50+ μm (0.002"+) | Abrasion resistance, surface hardness |
| Aerospace Components | Type I or Type III | 2-5 μm (Type I) / 50+ μm (Type III) | Fatigue resistance, tight tolerances, corrosion protection |
| Marine Applications | Type II or Type III | 25+ μm (0.001"+) | Saltwater corrosion resistance, sealed finish |
| Electronics Enclosures | Type II | 10-18 μm (0.0004"-0.0007") | Electrical insulation, EMI shielding compatibility |
| Food Processing Equipment | Type III (unsealed) | 25-50 μm (0.001"-0.002") | Cleanability, chemical resistance, FDA compliance |
When architects specify anodized aluminum extrusions for buildings, they're betting on decades of performance. According to A-Line Automation, architects choose anodized aluminum for exterior panels and interior design accents because of its ability to withstand outdoor elements while retaining visual appeal. But getting that performance requires specifying the right parameters.
For exterior applications like curtain walls, window frames, and storefronts, Type II anodizing with a minimum 18-micron (0.0007") coating thickness has become the industry standard. This specification provides the corrosion resistance needed to handle decades of rain, UV exposure, and temperature cycling. Coastal or industrial environments with salt spray or chemical pollutants may warrant even thicker coatings approaching 25 microns.
Color selection matters significantly for architectural projects. According to the Aluminum Anodizers Council, electrolytically deposited colors using tin, cobalt, or nickel offer superior lightfastness compared to organic dyes. Bronze tones produced through this method maintain their appearance for decades, while some organic dyes may fade noticeably within years of UV exposure. For projects requiring specific brand colors or vibrant hues, work with your anodizer to understand the expected fade characteristics before committing.
Interior applications allow more flexibility. Decorative trim, handrails, and fixtures typically face minimal environmental stress. Type II anodizing at 10-15 microns provides adequate protection while keeping costs reasonable. The full range of dye colors becomes available since UV stability is less critical indoors.
If you've worked with modular aluminum framing, you've encountered t extrusion profiles. These versatile components build everything from machine guards and workstations to automated assembly lines and clean room enclosures. According to industry sources, anodized aluminum's relationship with modular industrial designs makes it ideal for T-slot structural framing applications.
For standard t slot aluminum profile applications, Type II anodizing at 15-18 microns delivers the right balance of wear resistance, corrosion protection, and cost-effectiveness. The clear anodized finish commonly seen on industrial framing components protects against handling wear and light environmental exposure while maintaining the clean, professional appearance manufacturing facilities expect.
But when t aluminum framing faces heavier demands, specifications must escalate. Conveyor systems, automated guided vehicle tracks, and components subjected to repeated mechanical contact benefit from Type III hardcoat anodizing. According to technical specifications, hardcoat finishes achieve Rockwell C hardness ranging from 50 to 70, described as "file hard" with outstanding abrasion resistance in rubbing or sliding applications.
One important consideration for industrial applications: hardcoat finishes are often left unsealed intentionally. According to the Aluminum Anodizers Council, sealing can be detrimental to coating hardness. If your application prioritizes wear resistance over maximum corrosion protection, discuss unsealed hardcoat options with your provider.
Inevitably, you'll need to cut anodized extrusions to length or modify them for installation. Understanding how to cut extruded aluminum properly preserves both the finish quality and your cutting tools.
The anodized oxide layer is significantly harder than the base aluminum, which affects cutting behavior. Standard woodworking blades dull quickly and may chip the anodized surface. For clean cuts that maintain the finish:
For precision fabrication operations like drilling, milling, or CNC machining anodized parts, similar principles apply. Carbide tooling, appropriate feeds and speeds, and proper coolant application prevent finish damage while maintaining dimensional accuracy. Remember that Type III hardcoat is significantly harder than Type II, requiring adjusted machining parameters to prevent excessive tool wear.
Some applications fall outside standard architectural or industrial categories. Aerospace components often specify Type I chromic acid anodizing when fatigue resistance and tight dimensional tolerances matter most. According to the Aluminum Anodizers Council, chromic acid coatings are very resistant to corrosion, resulting in wide use on military hardware and products requiring excellent corrosion protection.
Consumer electronics and medical devices represent another specialty category. According to A-Line Automation, the electronics industry relies on anodized aluminum for smartphone casings and laptop chassis because of its eye-catching appearance and durability. Similarly, the medical field prefers anodized surfaces for their biocompatibility and ease of disinfection.
For marine applications where saltwater exposure is constant, extra precautions become necessary. Thicker Type II coatings with thorough sealing resist salt spray corrosion. Some specifiers choose Type III hardcoat for its denser oxide structure, though the darker natural color limits aesthetic options.
Matching specifications to applications requires understanding both what your project demands and what each anodizing option delivers. When in doubt, consulting with an experienced anodizing provider early in your design process prevents specification errors that become expensive to correct later. But beyond technical specifications, there's another dimension worth considering: how your anodizing choices affect sustainability and long-term environmental impact.
Beyond technical performance and aesthetic appeal, there's a compelling reason why architects, manufacturers, and procurement teams increasingly specify anodized aluminum extrusions: sustainability. In an era where environmental responsibility shapes purchasing decisions and building certifications, understanding the green credentials of your material choices matters more than ever. The good news? Anodized aluminum delivers on both fronts, combining exceptional performance with genuine environmental advantages that extend throughout the product lifecycle.
According to the Aluminum Anodizers Council, anodized aluminum is the "naturally green" material. Unlike surface treatments that rely on problematic chemicals or compromise recyclability, anodizing accentuates aluminum's inherent environmental benefits without diminishing them. But what exactly makes this electrochemical process stand out from alternatives?
Here's something that might surprise you: anodizing doesn't affect aluminum's legendary recyclability. While paints, powder coatings, and plated finishes can dramatically reduce the ability to recycle aluminum and increase processing costs, the anodized oxide layer creates no such barrier.
Recyclability is unaltered by anodizing, and no intermediate processing is needed for anodized metal to reenter the recycle chain, unlike thicker organic or plated metallic coatings.
This matters enormously when you consider the numbers. According to the Aluminum Association, approximately one-third of all aluminum produced in the United States today comes from recycled sources. That recycling saves roughly 95 percent of the energy required to produce aluminum from raw materials. When your anodized extrusions eventually reach end of life, they flow directly back into the recycling stream without additional processing steps or material loss.
The anodizing process itself carries a relatively benign environmental profile compared to alternatives. Consider these key advantages:
There's another environmental benefit worth noting. Aluminum-rich anodizing wastes often prove environmentally valuable, helping remove pollutants and settle solids in domestic sewage treatment processes. What might seem like waste from one industry becomes a resource for another.
Sustainability isn't just about recyclability. It's equally about extending product lifespan and reducing the consumption cycle that depletes resources and fills landfills. This is where anodized aluminum extrusions truly shine.
According to JM Aluminium, the anodized surface is extremely hard and thus preserves and extends the life of aluminum products. Unlike untreated metals that deteriorate over time, anodized surfaces resist oxidation and chemical wear. Coastal and industrial environments, which are prone to high humidity and corrosive agents, particularly benefit from this protection.
The practical implications cascade through every aspect of lifecycle sustainability:
Anodizing also reduces friction and increases lubricity, an advantage with fitted components and moving parts. According to the Aluminum Anodizers Council, this increased wear resistance means a longer life cycle, with hardcoat anodizing further improving resistance to physical forces.
For projects pursuing LEED certification or other sustainable building standards, anodized aluminum extrusions offer tangible advantages. According to Linetec, eco-friendly anodize contributes to LEED credit potential when utilizing recycled (secondary) billet. The improved aesthetic finish that eco-friendly anodizing provides on secondary billet means recycled aluminum can now be warranted with confidence that the finish will perform as intended.
Beyond certification points, anodized aluminum's combination of properties supports broader sustainable design objectives. The metal's excellent electrical conductivity, paired with the anodic coating's insulating properties, allows systems that save energy and materials. Aluminum can serve both structural and conductive purposes while the coating insulates circuits and preserves the structure, simplifying physical design and reducing wiring requirements.
When specifying materials for your next project, the environmental case for anodized aluminum extrusions extends well beyond marketing claims. From infinite recyclability without degradation to decades of maintenance-free performance, these characteristics represent genuine contributions to sustainable manufacturing and construction. But realizing these benefits requires working with suppliers who understand both the technical and environmental dimensions of quality anodizing, which brings us to the practical matter of specifying your requirements effectively.
You've selected the right anodizing type, determined your color preferences, and matched specifications to your application. Now comes the step that separates smooth projects from frustrating ones: communicating your requirements clearly to manufacturers. Sounds straightforward? In practice, incomplete or ambiguous anodized aluminum specifications cause more delays, rejections, and cost overruns than any technical challenge. Bridging the gap between what you need and what your supplier understands requires speaking the same language.
The good news is that effective specification doesn't require becoming an anodizing expert. It requires knowing which details matter, how to document them, and what questions to ask before production begins. Whether you're ordering a black aluminum h channel for architectural trim or custom anodized extrusion for industrial equipment, these principles apply universally.
When preparing your order documentation, include these key specification elements to prevent misunderstandings:
One detail that catches many buyers off guard: formal MIL-A-8625 certification costs significantly more than standard processing. According to industry sources, certification requires destructive testing procedures including salt spray and coating weight analysis, adding approximately $1,500 and 3-4 weeks to obtain results. If you need documentation but not full certification, discuss alternative compliance letters that compare standard anodizing to specification requirements without the testing expense.
Here's a critical consideration for precision parts: anodizing changes your dimensions, and failing to account for this creates parts that don't fit. According to Euro Machining, anodizing is a conversion coating where approximately 50% of the coating thickness penetrates the surface while the other 50% builds outward.
For a standard Type II anodize, expect dimensional growth of 0.0005" to 0.001" per surface. On a hole or bore, this means the diameter shrinks by twice the outward growth. On external dimensions, overall width increases by twice the per-surface growth. Type III hardcoat with 0.002" coating thickness creates even more significant dimensional shifts.
Practical guidelines for managing dimensional changes:
How do you verify that delivered parts meet your anodized aluminum specifications? Establishing inspection criteria upfront prevents disputes during acceptance.
Common verification methods include coating thickness measurement using eddy current methods (ASTM B244) for production line checks, or cross-sectional microscopy (ASTM B487) for definitive results. Seal quality verification through dye stain testing (ASTM B136) confirms that pores are properly closed. For demanding applications, salt spray testing (ASTM B117) validates long-term corrosion resistance.
For color-critical applications, establish a three-sample range showing light, target, and dark acceptable limits before production begins. This prevents subjective disagreements about whether delivered parts match expectations.
The complexity of anodizing specifications highlights why working with experienced manufacturers matters. Suppliers who offer integrated extrusion and finishing capabilities can manage the entire process, ensuring that alloy selection, profile design, machining tolerances, and anodizing parameters work together seamlessly.
Manufacturers like Shengxin Aluminium provide end-to-end support from die development through anodizing, with capabilities including custom anodizing colors like Champagne and Rose Gold. With over 30 years of industry experience and a technical team that understands how extrusion design affects anodizing outcomes, they can identify potential problems before production begins rather than after parts are rejected.
When evaluating potential suppliers for custom anodized extrusion projects, look for these capabilities:
Clear specifications combined with experienced manufacturing partners prevent the miscommunications that derail projects. With your requirements properly documented and a capable supplier engaged, you're positioned to receive anodized aluminum extrusions that meet both your technical requirements and quality expectations.
You've now explored the complete landscape of anodized aluminum extrusion, from the electrochemical science behind the process to the practical specifications that determine success. But knowledge without action remains theoretical. The real value comes when you apply these insights to your next project, making decisions that deliver lasting performance rather than costly compromises.
Whether you're sourcing industrial anodized aluminum for manufacturing equipment or specifying architectural finishes for a landmark building, the path forward requires matching your specific requirements to the right combination of anodizing type, color, and processing parameters. Let's consolidate what you've learned into actionable guidance.
Before placing your next order, work through this decision checklist to ensure you've addressed every critical factor:
Working through this checklist before engaging suppliers prevents the specification gaps that cause delays and rejected parts. Each decision builds on the others, creating a complete picture of what you need and how to communicate it effectively.
Even perfect specifications require capable execution. According to industry outlook reports, companies are increasingly consolidating suppliers to reduce risk, improve communication, and accelerate time to market. The shift reflects a broader expectation for anodized aluminum suppliers to deliver turnkey manufacturing rather than fragmented services.
What should you look for in a manufacturing partner? The ability to manage the entire process, from die development through extrusion, machining, and surface treatment, under one roof eliminates handoff problems between separate vendors. When your extrusion supplier also controls anodizing, they can optimize alloy selection, profile design, and processing parameters to work together seamlessly.
Shengxin Aluminium exemplifies this integrated approach. With 35 advanced extrusion presses ranging from 600T to 5500T capacity and comprehensive in-house anodizing capabilities, they manage every production step from initial die development through finished, anodized profiles. Their aluminum profile finishing services include specialty anodizing colors like Champagne and Rose Gold alongside standard clear, black, and bronze finishes.
What sets experienced custom aluminum extrusion manufacturers apart goes beyond equipment. Over 30 years of industry experience translates to technical teams who understand how extrusion design affects anodizing outcomes, who can identify potential problems during design review rather than after production begins. This proactive approach prevents the costly corrections that arise when extrusion and finishing are treated as separate, disconnected processes.
For projects requiring precision and quality, look for partners who offer:
Looking ahead, anodized aluminum extrusion applications continue expanding across industries. According to industry forecasts, demand for lightweight, sustainable, and highly customizable solutions drives growth in aerospace interiors, minimally invasive medical devices, military equipment, and compact industrial systems. The combination of aluminum's strength-to-weight ratio, anodizing's protective capabilities, and extrusion's design flexibility positions this material system for continued relevance.
Sustainability pressures and cost-reduction initiatives are pushing manufacturers toward near-net-shape extrusion processes that reduce waste and streamline production. As quality standards tighten across aerospace, medical, and architectural markets, the value of working with experienced partners who understand both extrusion and finishing only increases.
Whether you're designing the next generation of electronic enclosures, specifying window systems for sustainable buildings, or engineering precision components for demanding industrial environments, anodized aluminum extrusion delivers the performance, aesthetics, and longevity your projects demand. The knowledge you've gained throughout this guide positions you to make informed decisions that serve your applications for decades to come.
Ready to explore custom anodized extrusion solutions for your next project? Connect with Shengxin Aluminium's technical team to discuss your requirements and discover how integrated extrusion and finishing capabilities can bring your vision to life.
Yes, extruded aluminum is ideal for anodizing. The process involves submerging cleaned aluminum extrusions in an acid electrolyte bath while passing electrical current through the solution. This creates a durable oxide layer that becomes integral to the metal itself. Alloys like 6063 and 6061 are particularly well-suited for anodizing, producing excellent surface finishes and accepting dyes beautifully for architectural and industrial applications.
The 720 rule is an industry-standard calculation used to determine anodizing parameters for achieving a desired coating thickness. It helps technicians establish the relationship between current density, time, and oxide layer thickness. While effective for many common aluminum alloys like 6063, the rule may require adjustment for alloys with high concentrations of copper, zinc, or silicon, where non-aluminum constituents affect the oxide formation rate.
Aluminum 6063 is widely considered the best alloy for both extrusion and anodizing. It offers excellent extrudability, produces smooth surface finishes, and accepts anodizing dyes consistently. Aluminum 6061 provides higher strength but is slightly more challenging to extrude. For optimal color matching and clear anodized finishes, alloys 5052 and 3003 also perform exceptionally well due to their lower impurity content.
Type II sulfuric acid anodizing produces 1.8-25 micron thick coatings ideal for decorative and architectural applications, accepting vibrant dye colors including black, bronze, and custom shades. Type III hardcoat anodizing creates 25-150 micron thick coatings with hardness ratings of 65-70 Rockwell C, suitable for wear-critical industrial components. Type II is cost-effective and versatile, while Type III delivers maximum abrasion resistance but limits color options to natural dark gray or black.
Anodizing changes part dimensions because approximately half the oxide layer penetrates into the aluminum while half builds outward. For Type II anodizing, expect 0.0005-0.001 inches growth per surface. Type III hardcoat with 0.002-inch thickness adds approximately 0.001 inches per surface. Additionally, pre-treatment etching removes 0.0001-0.0006 inches per surface. Specify whether critical dimensions apply before or after finishing to ensure proper fit.


 Інтернет-сервіс
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 Українська
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Việt