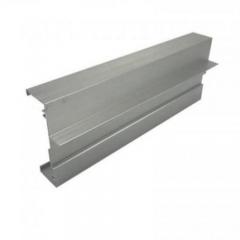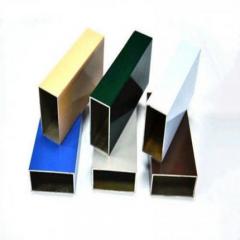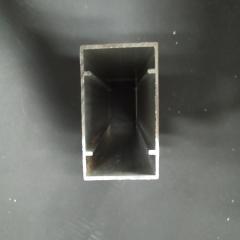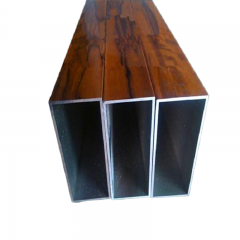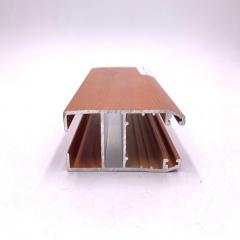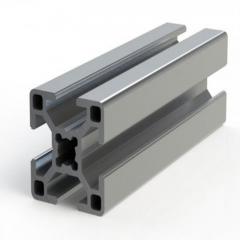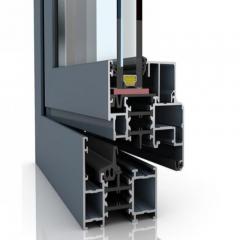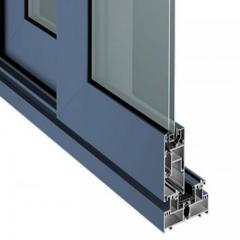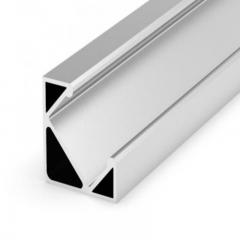
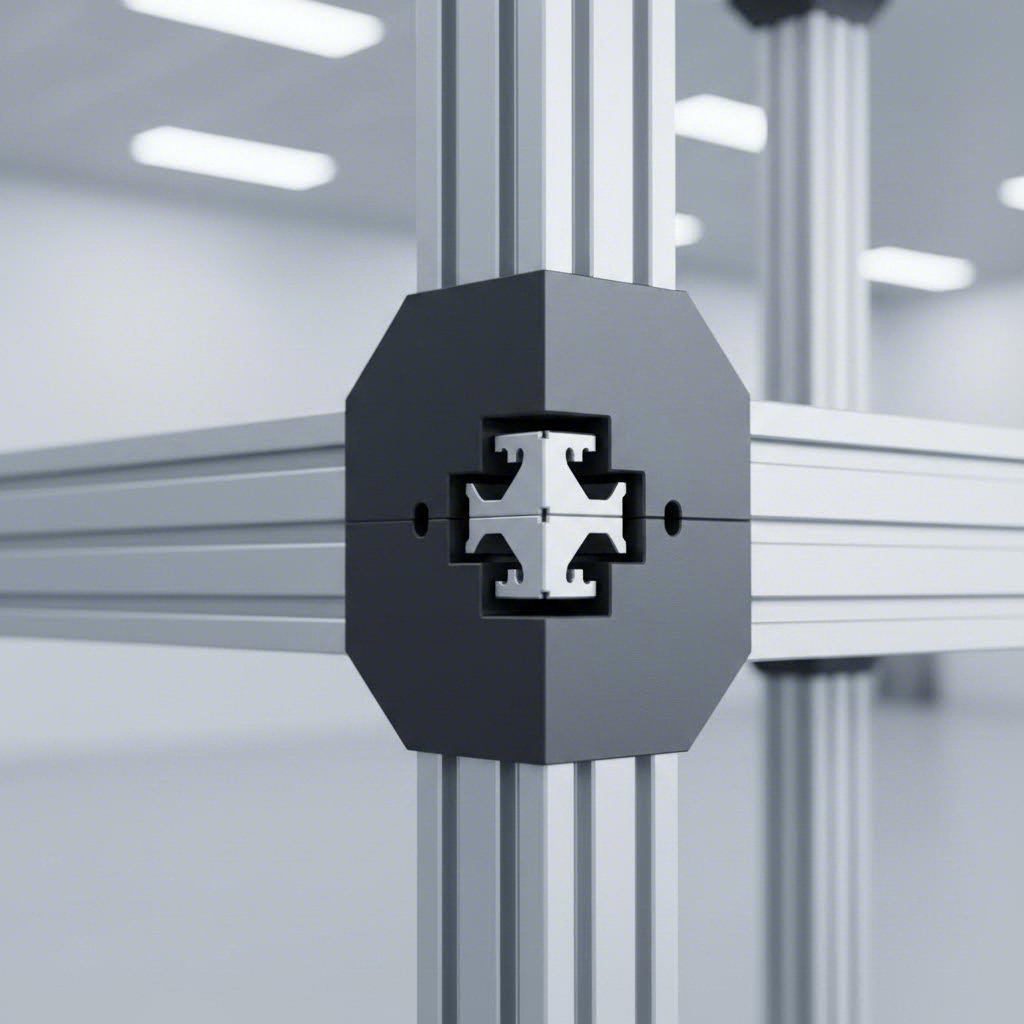
Ever wondered how those sleek, precisely shaped aluminum profiles in machinery frames, workstations, and display structures come to life? The answer lies in a fascinating manufacturing process that transforms raw metal into virtually any shape you can imagine. Aluminum frame extrusions are structural components created by forcing heated aluminum through specially designed dies, resulting in consistent cross-sectional profiles that form the backbone of modern modular framing systems.
Think of it like squeezing toothpaste from a tube—except the "tube" is a powerful hydraulic press, and the opening is a custom-shaped steel die. The result? Extruded aluminum profiles with remarkable precision, strength, and versatility that traditional fabrication methods simply cannot match.
The aluminum extrusion process begins with a cylindrical aluminum billet—essentially a large "log" of raw aluminum alloy. Here's how manufacturers transform this raw material into finished profiles:
The beauty of this process lies in its consistency. Once you aluminum extrude a profile through a die, every inch of that extrusion maintains identical dimensions and properties. This precision is what makes these profiles ideal for building modular framing systems where components must connect seamlessly.
You might ask: why aluminum instead of steel or other metals? The answer comes down to an unbeatable combination of properties that make aluminum extrusion profiles the preferred choice for structural framing applications.
Unlike welding, cutting, or bending metal sheets, the extrusion process enables manufacturers to create complex hollow shapes, integrated mounting channels, and intricate geometric patterns in a single continuous operation—shapes that would be impossible or prohibitively expensive to achieve through traditional fabrication.
Consider these key advantages of extruded aluminum framing:
The extrusion extrusion process also supports secondary operations like heat treatment, anodizing, and powder coating—allowing manufacturers to enhance mechanical properties and customize aesthetics. Whether you need a simple workbench frame or a complex machine enclosure, aluminum extrusions provide the building blocks for structures that are strong, lightweight, and infinitely adaptable.
You've decided to build with aluminum t slot profiles—but then you open a supplier catalog and encounter a wall of cryptic numbers, abbreviations, and technical jargon. Sound familiar? Terms like "4040," "T-nut," and "moment of inertia" can make even straightforward projects feel overwhelming. Let's decode this terminology so you can confidently navigate any product listing or specification sheet.
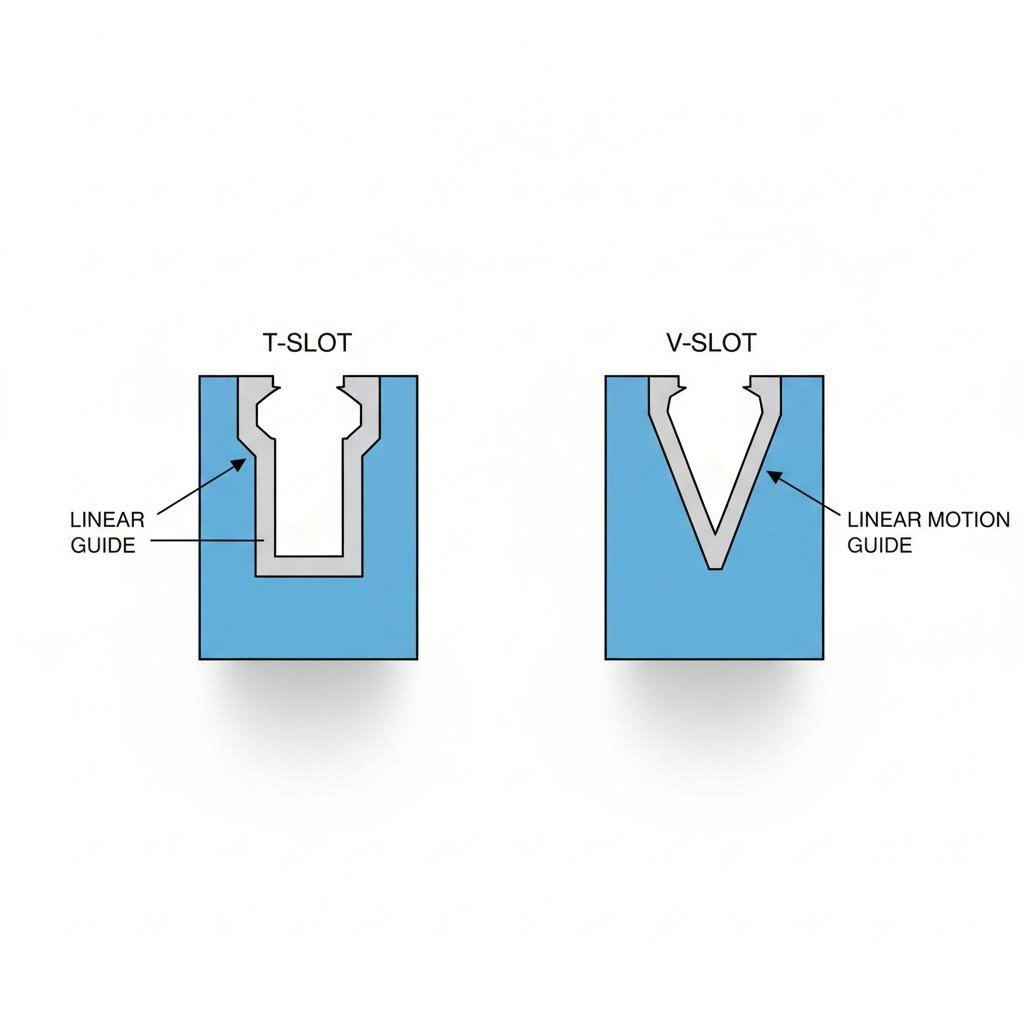
When browsing aluminum framing options, you'll immediately encounter two dominant profile styles: T-slot and V-slot. Understanding their differences helps you choose the right system for your application.
T-Slot profiles feature the signature "T" shaped groove running along one or more sides of the extrusion. This t slotted rail design has been the industry standard for decades, used in everything from machine enclosures to CNC machines, 3D printers, and industrial robots. The T-channel aluminum design accepts specialized hardware—like T-nuts and drop-in fasteners—that slide into the groove and lock components in place at any position along the profile.
V-Slot profiles incorporate the same T-slot functionality but add V-shaped grooves along the corners. These V-grooves serve as linear rails, allowing special V-wheels to roll smoothly along the profile. This makes v slotted aluminum insert systems ideal for linear motion applications like 3D printer axes, CNC gantries, and sliding mechanisms—all without requiring separate linear rail hardware.
Here's how these two systems compare:
| Feature | T-Slot | V-Slot |
|---|---|---|
| Primary Function | Structural framing and modular assembly | Structural framing plus integrated linear motion |
| Groove Shape | T-shaped channels on faces | T-shaped channels plus V-grooves on corners |
| Linear Motion | Requires separate rail systems | Built-in V-wheel compatibility |
| Hardware Compatibility | T-nuts, brackets, drop-in fasteners | Same as T-slot plus V-wheels |
| Best For | Workstations, enclosures, static structures | 3D printers, CNC machines, motion systems |
Those confusing four-digit numbers like "2040" or "4040" actually follow a logical naming convention. Once you crack the code, selecting the right t slot rail becomes straightforward.
According to 80/20's naming convention guide, profile names typically follow this pattern:
[Series Number]-[Profile Width]x[Profile Height]-[Additional Features]
For most tslots you'll encounter:
So when you see "4040," you're looking at a 40mm x 40mm square profile. A "2040" designation indicates a 20mm x 40mm rectangular profile—twice as tall as it is wide. This straightforward system lets you instantly visualize profile dimensions from the model number alone.
Profile series also indicate slot width and load capacity. Common series include:
Beyond profile types and sizes, you'll encounter specialized terms throughout your project. Here's your essential aluminum t channel vocabulary:
| Term | Definition |
|---|---|
| T-Nut | A fastener with a T-shaped cross-section that slides into T-slot channels and provides threaded mounting points |
| Profile Series | The base dimension (20mm, 40mm, 45mm) that determines slot size and overall scale of the extrusion system |
| Fastening Channel | The T-shaped groove running along a profile's face where hardware connects |
| Moment of Inertia | A measurement of a profile's resistance to bending—higher values indicate greater stiffness under load |
| Drop-In T-Nut | A T-nut that can be inserted anywhere along an assembled profile without sliding from the end |
| Roll-In T-Nut | A T-nut that must be inserted from the profile's end and slid into position before assembly |
| Gusset | A triangular or angled bracket that reinforces corner connections |
You'll also encounter these common industry abbreviations:
With this terminology foundation in place, you're ready to tackle the next critical decision: choosing the right aluminum alloy for your specific application requirements.
You've mastered the terminology and understand how profiles are named—but here's a question that trips up many builders: does the alloy actually matter? The short answer is yes, and choosing the wrong one can mean the difference between a frame that performs flawlessly for decades and one that fails under load or corrodes prematurely.
When shopping for extruded aluminium profiles, you'll encounter alloy designations like 6063, 6061, and temper codes like T5 or T6. These aren't just random numbers—they define the mechanical properties, workability, and ideal applications for each material. Let's break down what these designations mean for your project.
If there's a "workhorse" alloy in the aluminium extrusion world, it's 6063. Often called "architectural aluminum," this alloy dominates the framing industry for good reasons that go beyond just tradition.
According to Gabrian International, 6063 is the most popular aluminum alloy for extrusions. It belongs to the 6000 series, meaning its primary alloying elements are magnesium (0.45-0.9%) and silicon (0.2-0.6%). These additions create an alloy optimized specifically for the extrusion process.
What makes 6063 ideal for frame applications?
For most modular framing projects—workstations, enclosures, display structures, and light-to-medium-duty machine frames—aerospace-grade 6063 aluminum provides more than adequate strength while delivering the finish quality and corrosion resistance your application demands.
While 6063 handles the majority of framing applications, some projects demand higher strength. That's where 6061 enters the picture. Often called "structural aluminum," 6061 contains slightly higher magnesium (0.8-1.2%) and silicon (0.4-0.8%) content, resulting in improved mechanical properties.
Here's how these alloys compare across key performance factors:
| Property | 6063-T5 | 6063-T6 | 6061-T6 |
|---|---|---|---|
| Tensile Strength | ~185 MPa | ~240 MPa | ~310 MPa |
| Yield Strength | ~145 MPa | ~215 MPa | ~276 MPa |
| Extrudability | Excellent | Excellent | Good |
| Surface Finish | Very smooth | Very smooth | Good |
| Corrosion Resistance | Very good | Very good | Good |
| Machinability | Moderate | Moderate | Excellent |
| Weldability | Good | Good | Good |
| Relative Cost | Lower | Lower | Moderate |
Notice the temper designations (T5, T6) in the table? These codes indicate how the aluminum was heat-treated after extrusion, and they significantly impact performance.
According to EOXS, here's what each temper means:
Design note: T6 tempered aluminum offers maximum strength, but its lower ductility means tight bends require careful planning to prevent cracking. If your design involves post-fabrication bending or forming, consider T5 or T4 tempers instead.
Choosing between alloys doesn't have to be complicated. Consider these application scenarios:
Choose 6063-T5 or 6063-T6 when:
Choose 6061-T6 when:
Here's the practical reality: for most aluminum frame extrusion projects, 6063 in T5 or T6 temper provides the ideal balance of strength, workability, and value. Reserve 6061-T6 for applications where you've calculated specific load requirements that exceed what 6063 can handle—or when you need an aluminum plate or thicker structural component rather than an extruded profile.
With your alloy selection clarified, the next step is determining which profile size matches your project's actual load requirements and performance expectations.
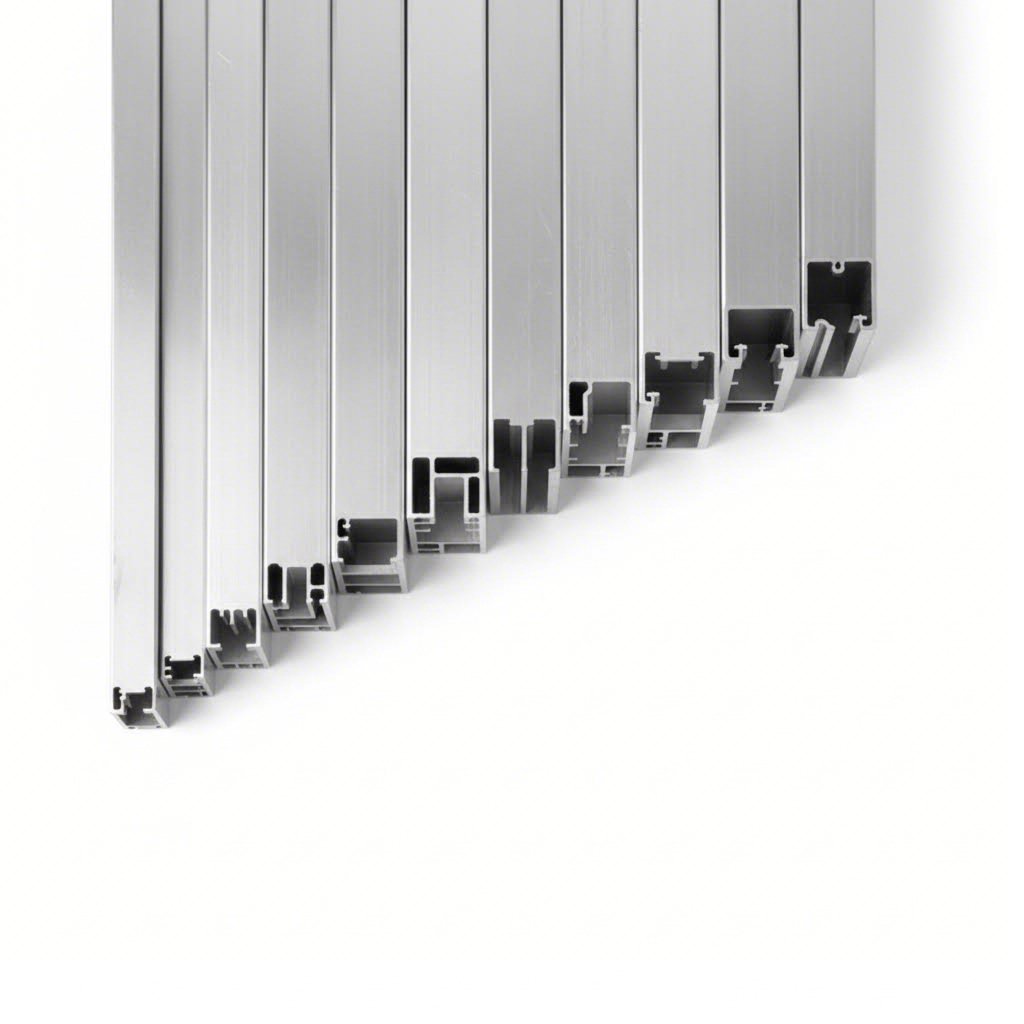
You've selected your alloy and understand the terminology—but now comes the question that determines whether your frame stands strong or sags under load: which profile size do you actually need? This is where many builders either over-engineer (wasting money on unnecessarily heavy profiles) or under-spec (ending up with a structure that deflects or fails).
The good news? Selecting the right aluminum extrusion profile isn't guesswork. By understanding how profile series, geometry, and load capacity relate to real-world applications, you can confidently match extruded aluminum profiles to your specific requirements.
Profile series numbers—20, 30, 40, 45, and 80—aren't arbitrary. They represent the base dimension in millimeters and directly correlate with load-bearing capacity, rigidity, and appropriate applications. Think of it this way: just as you wouldn't use a stepladder to reach the roof or scaffolding to change a light bulb, different profile sizes serve different structural demands.
According to comparative analysis of aluminum extrusion specifications, larger cross-sections provide exponentially greater rigidity and load capacity—not just proportionally more. An 80 20 aluminum profile doesn't just handle twice the load of a 4040; it handles significantly more due to the increased moment of inertia from its larger geometry.
Here's how the major profile series compare across key specifications:
| Profile Series | Base Dimension | Typical Slot Width | Relative Load Capacity | Common Use Cases |
|---|---|---|---|---|
| 20 Series | 20mm x 20mm | 5-6mm | Light (baseline) | 3D printer frames, small fixtures, electronics enclosures, prototypes |
| 30 Series | 30mm x 30mm | 6-8mm | Light-Medium (~2x baseline) | Display structures, workbench accessories, medium fixtures |
| 40 Series | 40mm x 40mm | 8-10mm | Medium-Heavy (~4x baseline) | Industrial workstations, machine guards, assembly frames |
| 45 Series | 45mm x 45mm | 10mm | Heavy (~5x baseline) | Heavy machinery bases, large enclosures, structural supports |
| 80 Series | 80mm x 80mm | 10-12mm | Maximum (~12x+ baseline) | CNC machine bases, automated production lines, large-scale structures |
Notice that load capacity doesn't scale linearly with size. This happens because structural rigidity depends on the moment of inertia—a property that increases dramatically as you move material farther from the profile's center. A 4040 profile isn't just "twice as strong" as a 2020; the physics of beam mechanics mean it resists bending far more effectively.
Within each series, you'll encounter different aluminum extrusion shapes offering varying levels of versatility and strength. The number and arrangement of T-slots significantly impact both connection options and structural performance.
Single-slot profiles feature T-channels on only one or two faces. These work well when you need connections only in specific directions—like a horizontal beam that mounts components on top but doesn't need side attachments.
Quad-slot profiles (the most common configuration) provide T-channels on all four sides. This geometry offers maximum flexibility for attaching brackets, panels, and accessories from any direction. The distributed material also provides balanced strength across multiple load directions.
When considering extruded aluminum sizes, also pay attention to rectangular versus square profiles:
Pro tip: A 2040 rectangular profile oriented with its 40mm dimension vertical provides significantly more resistance to downward deflection than a 2020 square profile—often at minimal additional cost.
The most practical approach to profile selection? Start with your application category and work backward to the appropriate aluminum extruded shapes. Here's how common projects typically align with profile weight classes:
Light-Duty Applications (20-30 Series):
Medium-Duty Applications (30-40 Series):
Heavy-Duty Applications (45-80 Series):
According to 80/20 load capacity specifications, even within a single profile series, variations like "Standard," "Lite," and "Ultra-Lite" versions offer different wall thicknesses and weight ratings. Standard profiles maximize strength, while Lite versions reduce weight and cost for applications that don't require maximum capacity.
When you're unsure which aluminum extrusion profile to choose, consider these decision factors:
For most DIY and light industrial projects, 40-series 80/20 aluminum profiles hit the sweet spot between capability and cost. They're strong enough for serious structural work, compatible with a vast ecosystem of accessories, and widely stocked for quick availability. Reserve 20-series for genuinely lightweight applications, and step up to 45 or 80-series only when calculations or experience indicate you need the extra capacity.
With your profile size determined, the next consideration is how different framing system approaches—T-slot, Quick Frame, or pipe-and-joint—affect your project's flexibility, assembly speed, and long-term adaptability.
You've selected your profile size and alloy—but here's a decision that shapes your entire build experience: which framing system should you actually use? While t slotted aluminum extrusions dominate the market, they're not the only option. Understanding how different modular systems compare helps you choose the right approach for your specific application, budget, and long-term flexibility needs.
Think of it like choosing between building blocks: LEGO, Erector Sets, and Lincoln Logs all create structures, but each system offers distinct advantages depending on what you're building. The same logic applies to extruded aluminum framing systems.
T-slotted framing has been the industry standard since the 1970s, and for good reason. The signature T-shaped channels running along each profile face create a universal mounting system that accepts standardized hardware—T-nuts, brackets, and fasteners that slide into position anywhere along the extrusion.
What makes t-slot framing the go-to choice for most industrial and DIY applications? According to industry analysis from JHFoster, the built-in modularity allows you to assemble, disassemble, and reassemble structures without starting from scratch. Need to add a shelf to your workstation next month? Simply slide in new T-nuts and bolt on the components—no drilling, welding, or permanent modifications required.
The t slotted framing ecosystem extends far beyond just profiles. Major manufacturers like 80/20, Bosch, and Item offer thousands of compatible accessories:
This extensive accessory library means you can build virtually anything—machine enclosures, workstations, conveyor supports, safety guarding—using off-the-shelf components that connect seamlessly with your modular aluminum framing.
While T-slot systems excel in precision applications, alternative approaches serve different priorities. Pipe-and-joint systems (like Flexpipe, Creform, or LeanTek) and proprietary quick-frame solutions each carve out distinct niches in the manufacturing landscape.
Pipe-and-joint systems use steel or aluminum tubes connected by specialized fittings at junction points. According to Flexpipe's comparative analysis, these systems perfectly embody Lean Manufacturing principles—they're simple to assemble, highly customizable, and significantly more affordable than T-slot alternatives for many applications.
AngleLock systems represent a newer alternative that addresses some of T-slot's limitations. As explained by AngleLock's engineering team, traditional T-slot joints rely on friction to maintain alignment, which can lead to loosening under vibration or dynamic loads. AngleLock's angled bolt system creates a mechanical lock with five planes of anchoring, resulting in joints that actually tighten under load rather than loosening over time.
Here's how these major framing systems compare across critical project factors:
| Factor | T-Slot Framing | AngleLock / Quick Frame | Pipe & Joint |
|---|---|---|---|
| Adjustability | Excellent—hardware positions anywhere along slots | Good—precise but less repositioning flexibility | Very good—fittings allow angular adjustments |
| Assembly Speed | Moderate—alignment requires careful adjustment | Fast—self-aligning brackets, ~50% faster than T-slot | Very fast—simple push-fit connections |
| Precision | Good—but can shift during tightening | Excellent—mechanical lock prevents movement | Moderate—1" intubation tolerance |
| Load Capacity | High—profiles up to 35,000 psi tensile strength | Very high—uses full profile strength potential | Moderate—up to 2,000 lbs maximum |
| Maintenance Needs | Regular bolt retightening in dynamic applications | Minimal—joints self-tighten under load | Low—simple structure, few failure points |
| Up-Front Cost | Moderate | Higher | Lower (~30% less than T-slot) |
| Long-Term Cost | Higher (maintenance, potential replacements) | Lower (extended service life) | Lowest for appropriate applications |
| Accessory Ecosystem | Extensive—thousands of components available | Limited—single manufacturer | Good—multiple vendors, simpler options |
So which approach makes sense for your project? The answer depends on what you're building and what factors matter most.
Regardless of which system you choose, all modular aluminum framing approaches share a critical advantage over traditional welded steel construction: adaptability. Welded frames are permanent—modifying them requires cutting torches, grinders, and re-welding, often costing as much as building new.
Modular systems flip this equation. As production needs evolve, workstations can be reconfigured, machine guards relocated, and entire assembly lines restructured using the same components. This flexibility isn't just convenient—it's increasingly essential in manufacturing environments where product cycles shorten and adaptability drives competitiveness.
For most applications involving robotics, automation, or precision requirements, t slotted aluminum extrusions remain the obvious choice. Reserve pipe-and-joint systems for flow racks, carts, workstations, and applications where rapid iteration and cost efficiency outweigh precision demands. And when your application involves significant vibration or dynamic loads where joint reliability is paramount, AngleLock-style mechanical locking systems warrant serious consideration despite their higher entry cost.
With your framing system selected, the next critical decision involves how you'll actually connect everything together—the fastening methods and hardware that transform individual profiles into rigid, reliable structures.
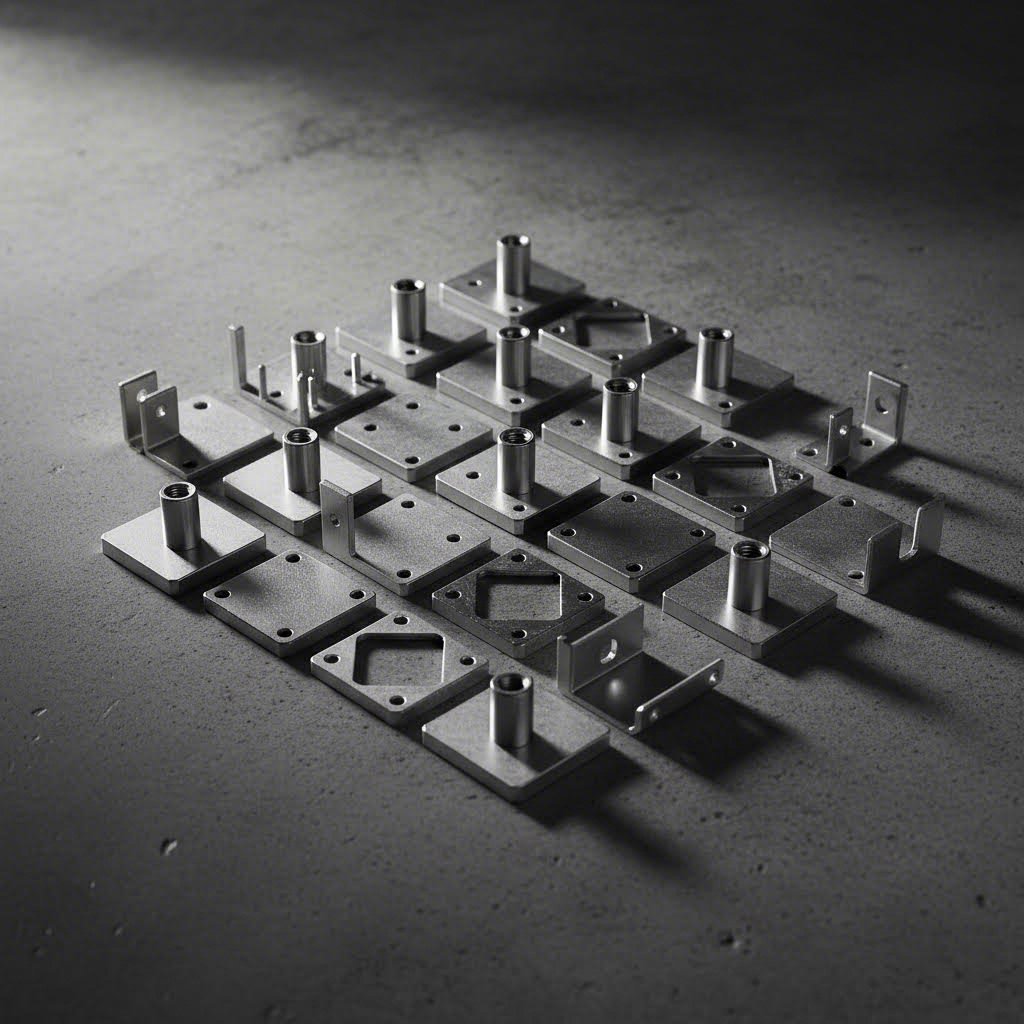
You've selected your profiles, chosen your framing system, and mapped out your design—but here's the reality check: your structure is only as strong as the connections holding it together. The fastening hardware you choose determines not just structural integrity but also assembly speed, adjustability, and the overall aesthetic of your finished build.
When it comes to aluminum frame systems, fasteners fall into two fundamental categories: internal and external. Understanding when to use each approach—and which specific hardware suits your application—separates professional-quality builds from wobbly disappointments.
Imagine you're building a machine enclosure that needs to look polished and professional. Do you want visible brackets cluttering every corner, or clean lines with hidden connections? That's the core trade-off between internal and external fasteners.
Internal fasteners work directly within the T-slot channels, creating connections that are largely or completely hidden from view. According to 80/20's fastener guide, these typically require machining—drilling access holes or tapping threads into the profiles—but the result is a sleek, uncluttered appearance with fewer exposed parts.
External fasteners mount on the outside of profiles, connecting pieces through brackets, plates, or gussets bolted into the T-slot channels. They're easier to implement (usually requiring no machining), simpler to adjust after assembly, and often provide stronger connections for heavy-duty applications.
Here's how these two approaches compare across key factors:
| Characteristic | Internal Fasteners | External Fasteners |
|---|---|---|
| Visibility | Hidden or recessed within profiles | Visible on profile exterior |
| Machining Required | Usually (access holes, tapping) | Rarely needed |
| Assembly Complexity | More planning required | Straightforward bolt-on installation |
| Adjustability | Limited once assembled | Easy to reposition along T-slots |
| Hardware Count | Fewer separate parts | More components (brackets, T-nuts, bolts) |
| Connection Strength | Good to excellent | Good to excellent (gussets add reinforcement) |
| Cost | Lower hardware cost, higher labor | Higher hardware cost, lower labor |
Within these two categories, you'll encounter specific hardware designed for different connection scenarios. Each type excels in particular applications—similar to how bolts for 4x4 posts differ from screws for metal studs based on the materials and loads involved.
| Fastener Type | Category | Key Advantages | Best Applications |
|---|---|---|---|
| Drop-In T-Nut | Internal | Installs anywhere without disassembly; spring-loaded for easy positioning | Adding accessories to assembled frames; retrofit mounting points |
| Roll-In T-Nut | Internal | Lower profile; stronger grip; more economical for planned assemblies | New builds where nut positions are predetermined before assembly |
| Anchor Fastener | Internal | Strongest internal connection; cam-lock mechanism creates lasting bond | Structural joints requiring maximum strength; frames with vibration exposure |
| Corner Bracket | External | Quick 90° connections; no machining; infinitely repositionable | Workstation frames; enclosures; applications needing frequent adjustment |
| Gusset | External | Triangular design adds rigidity; stronger than standard brackets | Heavy-load corners; frames supporting equipment weight; 4x4 brackets for reinforcement |
| Flat Joining Plate | External | Connects profiles in-line or parallel; infinite slot positioning | Extending frame lengths; mounting extruded aluminum rails side-by-side |
So which fasteners should you actually use? The answer depends on your priorities. Here's when each type excels:
Choose drop-in T-nuts when:
Choose roll-in T-nuts when:
Choose anchor fasteners when:
Choose corner brackets or gussets when:
Here's something many builders overlook: proper torque and thread engagement determine whether your connections hold firm or work loose over time. Under-tightened fasteners allow movement and vibration damage. Over-tightened fasteners strip threads or crack components.
For aluminum frame connections, follow these guidelines:
Pro tip: When using external brackets on extruded aluminum rails, tighten fasteners in a star pattern—alternating between opposite bolts—to ensure even pressure distribution and prevent bracket distortion.
With your fastening strategy established, the next step involves understanding how these profiles and connections come together across real-world applications—from industrial workstations to custom enclosures and everything in between.
You've mastered profiles, alloys, and fastening methods—but here's where theory meets practice: what can you actually build with aluminum structural framing? The answer might surprise you. The same 4040 profile that forms a CNC machine base can become a retail display fixture, safety enclosure, or precision linear motion system. It all comes down to creative design and understanding how modular components adapt to vastly different requirements.
Rather than thinking in product SKUs, let's explore applications the way builders actually approach them—by what they need to accomplish.
Walk through any modern manufacturing facility and you'll see aluminum frame extrusions everywhere. These profiles have become the backbone of industrial infrastructure—not because they're trendy, but because they solve real problems that welded steel simply can't address.
Workstation applications represent one of the largest use cases for modular aluminum framing. According to A-Line Automation's application guide, fabricating specific workstations for different applications becomes more straightforward and cost-effective by eliminating the need for welding, drilling, or other complicated processes. Consider these common implementations:
Machine safety guarding has evolved from an afterthought into a critical design element. As TSLOTS explains, keeping employees and equipment safe is the priority of almost any company—and the modular nature of T-slot profiles allows you to design guards that fit the machine rather than forcing machines to accommodate rigid guard designs.
Why does aluminum framing excel for safety applications?
Common machine guarding infractions—unmaintained guards, unstable ground fastening, incorrectly sized enclosures, and inadequate space for operators—all become easier to address when your framing system allows quick modifications.
Beyond the factory floor, aluminum frame extrusions serve applications ranging from retail environments to trade shows to cleanroom facilities. The same profiles protecting CNC operators can showcase products or create controlled environments for sensitive manufacturing.
Protective enclosures represent a natural extension of machine guarding concepts:
Display and architectural applications leverage the same structural advantages for aesthetic purposes:
The crossover between industrial and commercial applications highlights a key advantage: profiles designed to withstand factory conditions easily handle the lighter demands of retail and display environments while providing premium aesthetics.
Here's where aluminum frame systems reveal their engineering depth. Beyond static structures, specialized profiles support precision linear motion—the kind of movement required for CNC machines, 3D printers, automated inspection systems, and robotic positioning.
According to MiniTec's linear motion catalog, applications range from simple saw backstops to complex six-axis positioning systems. Common linear motion implementations include:
Linear motion applications require specific profile considerations beyond standard framing. V-slot profiles (discussed earlier) integrate linear rail functionality directly into the extrusion, allowing V-wheels to ride along precision-ground surfaces. For higher-precision requirements, aluminum tubing and profiles designed to mount dedicated linear rails provide even greater accuracy.
Key consideration: Linear motion applications demand tighter tolerances than structural framing. Specify profiles explicitly rated for linear motion use, and pay careful attention to parallelism when assembling multi-axis systems.
What truly sets aluminum frame extrusions apart is how the same profiles serve vastly different purposes through creative design. A manufacturer might use 4040 profiles for:
This versatility extends to industries beyond manufacturing. The automotive sector uses aluminum profiles for test fixtures and assembly aids. Aerospace applications include maintenance platforms and tooling structures. Even the home improvement space has embraced these profiles—DIY enthusiasts build everything from desk frames to custom storage solutions.
According to A-Line Automation, T-slot aluminum has found extensive use across various applications, from industrial machinery to homemade projects and furniture. The same robustness serving factory automation supports home automation systems, security solutions, and custom furniture construction.
Understanding these diverse applications helps you see beyond catalog listings to the possibilities your project might explore. The profiles, connectors, and accessories you've learned about aren't just industrial commodities—they're building blocks for structures limited only by imagination and engineering requirements.
With applications understood, the next consideration involves how surface treatments and finishing options can enhance both durability and aesthetics for your specific use case.
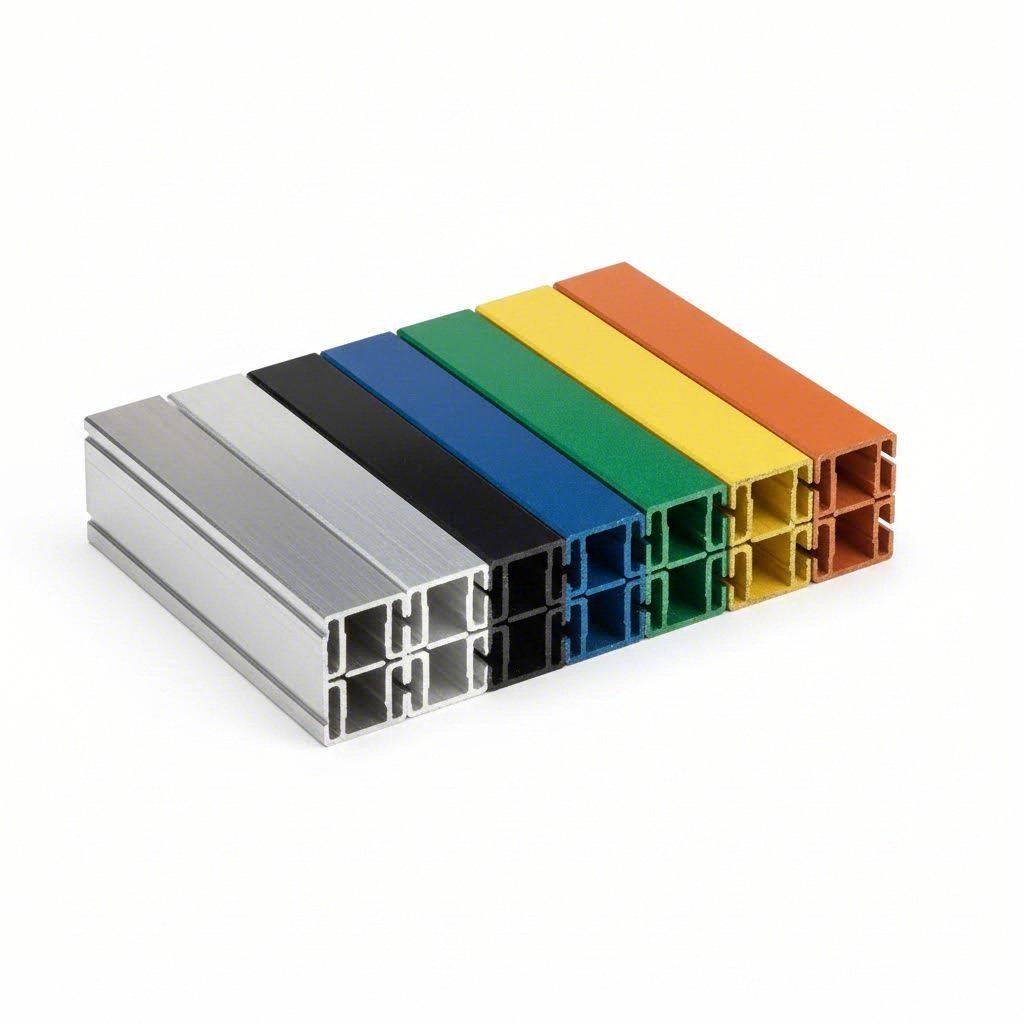
Your aluminum frame is structurally sound—but will it still look professional after years of use? Will it resist corrosion in humid factory environments or withstand outdoor exposure? The answer depends entirely on surface treatment. Raw aluminum develops a thin natural oxide layer, but for demanding applications, engineered finishes dramatically extend service life while opening up aesthetic possibilities you might not expect.
From classic silver anodizing to vibrant powder coats and specialized industrial treatments, understanding your finishing options helps you specify profiles that perform as beautifully as they function.
Anodizing remains the gold standard for aluminum surface treatment—and for good reason. This electrochemical process doesn't just coat the surface; it actually transforms it. According to Light Metals Coloring, anodizing creates a harder, thicker oxide layer that protects against wear and corrosion while allowing the surface to take on a broad range of colors.
Here's how the process works: technicians submerge your aluminium extruded profile in an electrolyte bath and apply electrical current, using the aluminum as the anode in the circuit. This triggers controlled oxidation that builds up a porous oxide layer far thicker than what forms naturally—and that porous structure is key to anodizing's versatility.
Anodized aluminum extrusions come in three main types, each suited to different applications:
Beyond protection, anodizing unlocks impressive color options. The porous oxide layer absorbs dyes before sealing, enabling colors ranging from subtle champagne and bronze tones to bold blacks, blues, and even rose gold finishes. Electrolytic coloring offers even greater durability by depositing metal salts into the pores—perfect for architectural applications exposed to UV and weather.
While anodizing can achieve tight shade tolerances, it doesn't behave like paint. Alloy composition, coating thickness, and process conditions influence final color—working with experienced finishers ensures predictable, repeatable results across production runs.
When your project demands vibrant colors, unique textures, or finishes that anodizing simply cannot achieve, powder coating enters the picture. According to Gabrian International's finishing comparison, powder coating offers brilliant colors and excellent durability—even when exposed to the elements.
Unlike liquid paint, powder coating is a dry application process. Technicians apply electrostatically charged powder particles to grounded aluminum profiles, then cure the coating in an oven where it melts into a uniform, solid layer. The result? A thick, durable finish available in virtually unlimited colors and textures—from smooth gloss to textured matte.
For the most demanding environments, advanced treatments go beyond standard finishes:
Choosing the right finish means balancing durability, aesthetics, and budget. Here's how the major surface treatments stack up:
| Finish Type | Durability | Color Options | Relative Cost | Best Applications |
|---|---|---|---|---|
| Clear Anodizing | Very good | Natural metallic silver | Low-Moderate | Standard aluminum extrusions, industrial frames, indoor equipment |
| Color Anodizing | Very good | Wide range (gold, bronze, black, custom) | Moderate | Architectural elements, consumer products, display structures |
| Hardcoat Anodizing | Excellent | Limited (typically dark gray/black) | Moderate-High | High-wear components, black aluminum extrusion for industrial use |
| Powder Coating | Very good | Unlimited colors and textures | Moderate | Outdoor equipment, architectural facades, colorful displays |
| PVDF Coating | Excellent | Wide range with superior color retention | Higher | Long-term outdoor exposure, architectural cladding |
| Micro-arc Oxidation | Exceptional | Limited | Highest | Extreme environments, high-temperature applications |
Your application determines which finish makes sense:
For complex projects requiring precise color matching across aluminum extrusion sizes or specialized treatments, partnering with manufacturers offering comprehensive surface treatment capabilities becomes essential. Facilities equipped for anodizing in custom colors, powder coating, PVDF, and micro-arc oxidation can deliver profiles matching exact project specifications—eliminating the coordination headaches of working with separate suppliers.
As an example of this integrated approach, Shengxin Aluminium's surface treatment services demonstrate how a complete aluminum extrusion supply chain—from die development through mass production and finishing—streamlines complex projects requiring multiple treatment options.
With surface treatments understood, you're ready to bring everything together: planning and executing your aluminum frame project from initial design through final assembly.
You've absorbed the knowledge—profiles, alloys, fasteners, finishes—but here's where it all comes together: actually building your aluminum extrusion frame. The difference between a project that assembles smoothly and one that turns into an expensive headache often comes down to planning decisions made before a single bolt gets tightened.
Whether you're designing a simple workstation or a complex automated production cell, thoughtful preparation transforms your extruded aluminum frame from concept to reality with fewer surprises, less rework, and better results.
Jumping straight into ordering profiles without proper planning is like building a house without blueprints—you might end up with a structure, but it probably won't be the one you wanted. According to SinoExtrud's load capacity analysis, aluminum extrusions often fail in real projects because load limits are guessed, not calculated. This leads to safety risks, wasted cost, and redesign work that no one wants.
Start with these fundamental questions before selecting a single component:
Load calculations deserve special attention. As the reference analysis explains, load capacity isn't a single number—it depends on how the profile is used, how it's supported, and how force is applied. Three distinct failure modes require evaluation:
Critical insight: If bending stress is below yield strength, that doesn't mean deflection can be ignored. Excessive deflection causes functional failure even when strength limits are met.
Before placing orders or cutting profiles, work through this comprehensive checklist to avoid common pitfalls:
For complex projects, consider using simulation tools to validate your design before committing to fabrication. According to structural engineering best practices, finite element analysis can predict structural performance accurately—but only when inputs, constraints, and material data are correct. Simulation should support basic calculations, not replace them.
Here's a reality many DIY builders discover: sourcing individual components from multiple suppliers often creates more problems than it solves. Mismatched tolerances, incompatible hardware, and coordination headaches quickly erode any perceived savings. For serious aluminum frame extrusion projects, finding the right manufacturing partner can make or break your timeline and budget.
According to comprehensive buyer guidance from Aluminum Processing Hub, evaluating potential partners requires probing several critical capabilities:
Die design and tooling expertise: Ask about in-house versus subcontracted tooling, expected die life, and maintenance practices. Request cross-sections and tolerance notes from recent jobs to verify fit with your requirements.
Press capacity and capability: Not all presses handle the same die complexity or part length. Larger presses accommodate wider cross-sections and help achieve tighter tolerances for long parts. When evaluating partners, look for facilities with extensive press capacity—operations ranging from 600T to 5500T presses can handle everything from delicate architectural profiles to heavy structural aluminum extrusions.
Secondary processing: Does the supplier perform CNC machining in-house? Capabilities for precise cutting, drilling, and bending eliminate the need to coordinate with additional vendors and ensure dimensional consistency across your aluminum extrusion frame kits.
Quality systems: Review inspection protocols, first-article inspection packages, and statistical process controls. Straightness and twist measurements matter especially for long profiles and linear motion applications.
MOQ flexibility: Discuss trial-run options, die amortization strategies, and phased production approaches that balance technical validation with budget constraints.
The best partners offer end-to-end support rather than just profile supply. Consider these evaluation criteria:
For an example of this integrated approach, Shengxin Aluminium's deep processing services demonstrate what comprehensive manufacturing support looks like in practice. With over 30 years of industry experience, 35 advanced extrusion presses (600T to 5500T capacity), and state-of-the-art CNC machining centers, they provide end-to-end support from die development through mass production—including extensive surface treatment options like anodizing in custom colors, powder coating, PVDF, and micro-arc oxidation. For custom aluminum extrusions, factory-direct pricing from established manufacturers often delivers better value than assembling components from multiple sources.
With proper planning, appropriate extruded aluminum frame components, and the right manufacturing partner, your project moves from concept to reality with predictable results. Remember these key principles:
The knowledge you've gained through this guide—from understanding extrusion fundamentals to selecting alloys, choosing profile sizes, comparing framing systems, and specifying finishes—provides the foundation for successful builds. Whether you're constructing a simple workbench or an elaborate automated production cell, aluminum frame extrusions offer the versatility, strength, and adaptability to bring your vision to life.
The company 80/20 named itself after Pareto's Law, the economic principle stating that 80% of results come from 20% of efforts. Italian economist Vilfredo Pareto (1843-1923) developed this concept. The name reflects the efficiency and versatility of their T-slot aluminum extrusion system, which allows builders to achieve significant results with minimal custom fabrication through modular, reconfigurable framing components.
Aluminum extrusion tooling typically costs between $500 to $5,000, making it significantly more affordable than die casting ($25,000+), roll forming ($30,000+), or stampings ($5,000+). Profile costs vary based on alloy type, size, complexity, and finish. Working with manufacturers offering factory-direct pricing and comprehensive services from die development through production often delivers better value than sourcing from multiple suppliers.
Common aluminum extrusion issues include dimensional inaccuracies from irregular cooling, worn dies, or incorrect extrusion speeds, leading to poor assembly fit. Surface defects like scratch marks or die lines result from improper lubrication or billet contamination. These challenges can be minimized by partnering with experienced manufacturers who maintain proper quality controls, use well-maintained equipment, and offer comprehensive inspection protocols.
The numbers indicate profile dimensions: 4040 is a 40mm x 40mm profile while 8020 refers to an 80mm x 20mm rectangular profile. The 8020 offers the highest strength-to-weight ratio for applications requiring maximum strength with minimal weight. The 4040 provides balanced strength suitable for most medium-load industrial applications. Profile selection depends on load requirements, span lengths, and application-specific needs.
6063 aluminum is the industry workhorse for frame extrusions due to excellent extrudability, superior surface finish, and very good corrosion resistance. It's ideal for workstations, enclosures, and light-to-medium-duty applications. For maximum structural strength, 6061-T6 offers higher tensile and yield strength, making it better suited for machine bases, heavy-duty frames, and applications involving dynamic loads or extensive machining.


 Інтернет-сервіс
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 Українська
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Việt